Custom Gym Bags for Sports Brands: The B2B Manufacturing, Material Engineering & Sourcing Playbook
The definitive B2B sourcing and manufacturing playbook for sports brands, fitness studio chains, and athletic retailers developing custom gym bags, duffels, and backpacks. Learn technical fabric selection, wet/dry compartment engineering, footwear ventilation tunnels, heavy-duty hardware specs, and OEM cost breakdowns.
In the modern global athletic apparel and fitness equipment industry, high-performance gym bags, sports duffels, and convertible training backpacks have evolved from basic functional accessories into premier brand-defining lifestyle statements.
For high-growth activewear DTC brands, boutique fitness studio franchises, CrossFit affiliates, collegiate athletic programs, and premium sporting goods retailers, a well-engineered custom gym bag represents one of the highest-margin, highest-visibility merchandise categories in their entire product catalog. Unlike seasonal apparel lines that rotate every quarter, a rugged, beautifully branded gym bag stays in active daily circulation for years—traveling from urban commuter trains and office desks to locker rooms, airport overhead bins, and outdoor training fields, generating continuous organic brand impressions.
However, transitioning from an initial design concept or aesthetic mood board to an industrially viable, commercially successful custom gym bag requires navigating complex engineering decisions. A sports bag operates under far harsher mechanical, environmental, and hygiene conditions than an ordinary commuter backpack:
- It must routinely carry 15 kg to 25 kg of dense weight—including cast-iron lifting chains, weightlifting belts, Olympic lifting shoes, stainless steel protein shakers, heavy recovery massage guns, and damp apparel.
- It must withstand intense internal biological humidity, sweat residue, and bacterial odor without developing mildew or seam rot.
- It must endure severe abrasive friction against textured gym floors, asphalt parking lots, metal locker corners, and airport luggage carousels.
- It must offer intelligent, rapid-access modular compartmentalization—isolating soiled footwear and damp swimwear from sensitive electronics, clean office attire, and nutritional supplements.
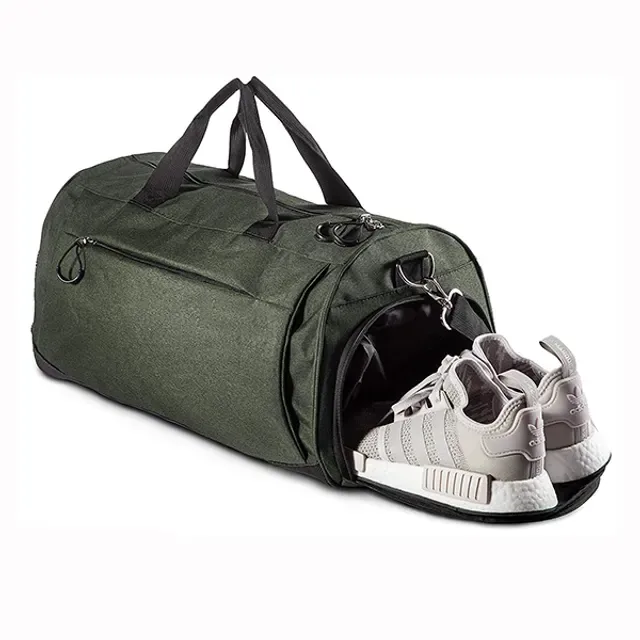
When sports brands partner with generic commercial luggage factories that lack specialized athletic bag engineering expertise, the results are all too familiar: shoe compartments with non-breathable linings that trap foul odors; shoulder strap anchor points that tear loose after three months of heavy lifting; cheap zipper teeth that burst open under lateral packing stress; and chemical coatings that peel or fail international consumer safety standards.
At Senszx, operating from our 10,000 m² owned manufacturing campus in Baigou, China with over 18 years of specialized OEM and ODM luggage and backpack production experience, we engineer and manufacture custom athletic bags for leading sports brands, international fitness chains, and commercial gear distributors worldwide.
This comprehensive B2B sourcing and manufacturing playbook provides athletic brand founders, product directors, technical apparel developers, and sourcing managers with an exhaustive, step-by-step engineering roadmap for developing, prototyping, costing, and manufacturing commercial-grade custom gym bags.
1. The Sports Brand Bag Market: Commercial Drivers & Sourcing Personas
To build a high-performing custom gym bag collection, brand directors must first understand the distinct commercial requirements, consumer usage patterns, and price-point expectations across different athletic customer segments.
1.1 The Four Core Buyer Personas in Athletic Bag Sourcing
Commercial sports bags are not one-size-fits-all products. Different end-users demand vastly different functional architectures, material selections, and aesthetic finishes:
| Sourcing Brand Persona | Primary End-Use Environment | Core Functional Demands | Typical Capacity (Liters) | Target Retail MSRP Price Tier |
|---|---|---|---|---|
| 1. High-Growth Activewear DTC Brands | Commuter-to-gym crossover, boutique studio fitness, urban lifestyle | Sleek minimalist exterior, hidden shoe tunnel, padded laptop sleeve, premium matte hardware | 28L – 38L | $75 – $145 |
| 2. Functional Fitness & Strength Chains | CrossFit boxes, powerlifting gyms, martial arts & MMA studios | Ultra-rugged 1000D/1680D fabric, external belt straps, laser-cut MOLLE webbing, 40 kg load rating | 45L – 65L | $95 – $185 |
| 3. Premium Studio Chains & Wellness Clubs | High-end yoga, Pilates, barre, luxury health spas | Dedicated external yoga mat carry straps, soft-touch waterproof nylon, thermal insulated shaker pockets | 22L – 32L | $85 – $165 |
| 4. Team Athletics & Collegiate Programs | High school / university sports teams, club soccer, aquatic centers | Oversized equipment volume, dual ventilated shoe gates, heavy-duty waterproof base, bold screen-print graphics | 50L – 80L | $45 – $85 |
1.2 Key Commercial Profitability & Retention Metrics
From a commercial merchandising perspective, custom athletic bags deliver outstanding business metrics for sports brands:
- High Average Order Value (AOV) Multipliers: An athletic duffel or convertible backpack carries an average retail price point of $65 to $150, allowing brands to bundle bags with core apparel lines (e.g., leggings, compression shirts, and lifting wraps) to instantly lift checkout cart values by 40% to 70%.
- Low Return Rates Compared to Sized Apparel: Sized athletic apparel (shorts, sports bras, footwear) routinely suffers from 20% to 35% e-commerce return rates due to fit discrepancies. Custom bags, as non-sized functional hardgoods, maintain industry-wide return rates below 2.5%, dramatically lowering reverse logistics costs and inventory write-downs.
- High Lifetime Brand Visibility: While an activewear t-shirt is typically worn once or twice a week, a premium gym bag is carried 5 to 7 days a week across multiple public transit and fitness environments, turning every customer into an active outdoor brand ambassador.
1.3 Strategic Positioning: How Leading Athletic Brands Build Iconic Gear Bags
When studying the market trajectory of iconic athletic gear bags developed by industry leaders such as Gymshark, Lululemon, Nike Training, Under Armour, and Rogue Fitness, clear architectural and merchandising patterns emerge:
- The Minimalist Aesthetic with Hidden Utility (Lululemon / Alo Yoga Style): Exterior surfaces prioritize clean, seamless contours, concealed reverse-coil zipper tracks, and whisper-quiet magnetic quick-access pockets, hiding heavy technical utility inside refined urban aesthetics.
- The High-Density Strength & Modularity Focus (Rogue Fitness / Nobull Style): Heavyweight 1000D Cordura exterior shells, oversized #10 YKK molded tooth zippers, exterior webbing compression straps for weightlifting belts, and Velcro loop fields for custom morale patches.
- The Multi-Modal Commuter Versatility (Gymshark Style): Ergonomic hybrid harnesses that convert effortlessly between horizontal hand-carry duffels and vertical ergonomic backpacks, featuring dedicated laptop compartments and high-contrast interior linings.
At Senszx, our technical product design team works alongside sports brand developers to translate these market trends into customized, brand-differentiated OEM/ODM product lines with protected proprietary tooling and signature hardware accents.
2. Core Gym Bag Silhouettes & Functional Architecture
Choosing the correct silhouette dictates the pattern cutting yield, assembly workstation layout, hardware requirements, and final production cost of your custom sports bag.
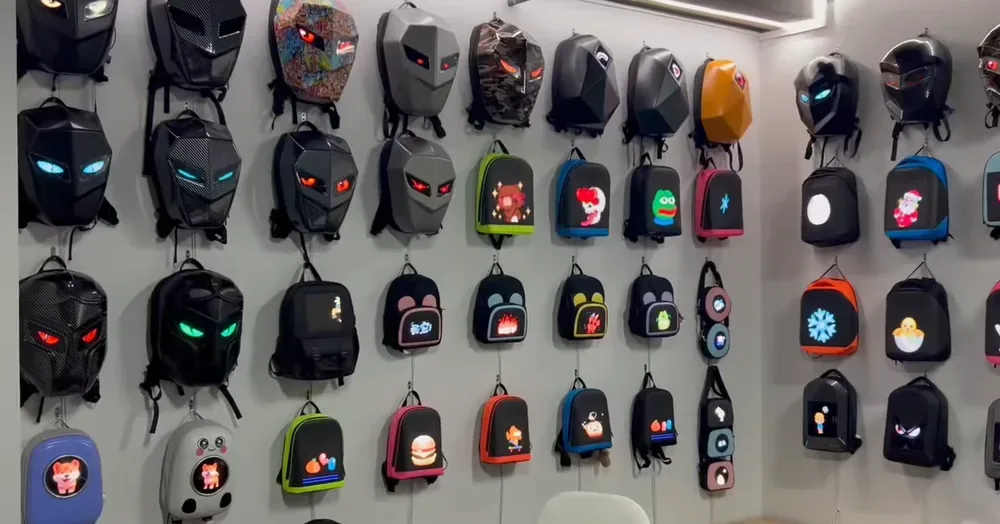
2.1 The Classic Cylinder / Barrel Duffel
The cylinder or barrel duffel is the time-tested foundation of athletic gear bags. Built with a continuous circular or U-shaped main zipper opening and round side end-caps, it maximizes raw internal packing volume while minimizing pattern cutting waste and assembly complexity.
- Best For: Team sports, collegiate athletic departments, lightweight promotional giveaways, and minimalist training kits.
- Manufacturing Complexity: Low to Moderate (18 to 26 individual cut panels).
- Key Structural Elements: Continuous 38 mm or 50 mm heavy-duty seatbelt webbing handles wrapping completely underneath the base panel to cradle the load, avoiding stress concentration along upper seam stitches.
2.2 The Convertible Hybrid Duffel-Backpack
The hybrid duffel-backpack is currently the fastest-growing silhouette in the premium urban activewear sector. It functions as a sleek horizontal duffel bag with dual hand grips, but features a zippered rear contour panel that deploys ergonomic, padded backpack shoulder straps complete with an adjustable sternum slider.
- Best For: Commuter athletes who bike, ride subways, or walk between office workplaces and after-hours fitness studios.
- Manufacturing Complexity: High (42 to 60 individual cut panels).
- Key Structural Elements: Concealed zippered stowage pockets for shoulder straps, heavy-duty anodized aluminum swivel carabiners, 3D breathable air mesh back cushioning, and a structured EVA-molded top lid.
2.3 The Compartmentalized Executive Gym Duffel
Designed for modern professionals who carry business technology and gym gear in a single organized carry-all. It abandons the single cavernous chamber in favor of a structured, multi-compartment architectural layout.
- Best For: Executive business professionals, corporate wellness programs, and premium travel athletes.
- Manufacturing Complexity: High (50 to 75 individual cut panels).
- Key Structural Elements: Dedicated 15.6" or 16" fleece-lined laptop and tablet compartment; isolated, heat-sealed waterproof wet/dry laundry pouch; collapsible ventilated shoe tunnel; magnetic quick-access passport and key fob pockets; and luggage trolley handle pass-through sleeves for airport travel.
2.4 The Studio Fitness Tote & Compact Crossbody Sack
Engineered specifically for boutique studio workouts (yoga, Pilates, barre, spin class) where users carry lightweight apparel, hydration, and personal accessories rather than bulky equipment.
- Best For: Women's activewear collections, boutique studio retail displays, and urban lifestyle crossover lines.
- Manufacturing Complexity: Moderate (24 to 34 cut panels).
- Key Structural Elements: Dual elastic or buckle-secured external webbing straps underneath or across the front panel designed to securely fasten a standard 6 mm yoga mat; thermal insulated exterior water bottle sleeves; and ultra-soft, water-repellent micro-weave nylon textiles.
| Silhouette Model | Capacity Range | Cut Panel Count | Key Structural Architecture | Target User Context |
|---|---|---|---|---|
| Classic Cylinder Duffel | 35L – 55L | 18 – 26 panels | Base-cradling continuous webbing wrap | Team sports, club athletics, minimalist gym kits |
| Convertible Hybrid Backpack | 32L – 48L | 42 – 60 panels | Deployable padded ergonomic shoulder harness | Multi-modal urban commuters, cycling athletes |
| Executive Multi-Pocket Duffel | 38L – 52L | 50 – 75 panels | Dedicated wet/dry/shoe/tech isolation | Business professionals, travel wellness athletes |
| Studio Yoga Fitness Tote | 20L – 30L | 24 – 34 panels | External yoga mat quick-anchor straps | Boutique studio fitness, Pilates, barre, yoga |
| Silhouette Feature & Parameter | Classic Cylinder Duffel | Convertible Hybrid Duffel-Backpack | Executive Multi-Compartment Duffel | Studio Fitness Yoga Tote |
|---|---|---|---|---|
| Standard Capacity | 40 Liters (52 × 28 × 28 cm) | 38 Liters (54 × 30 × 24 cm) | 45 Liters (56 × 32 × 28 cm) | 26 Liters (42 × 34 × 18 cm) |
| Typical Target Weight | 550 g – 750 g | 1,100 g – 1,450 g | 1,250 g – 1,600 g | 450 g – 680 g |
| Shoe Compartment | Side end-cap tunnel | Bottom expandable chamber | Side isolated ventilated tunnel | Internal drawcord shoe pouch |
| Laptop Protection | None / Optional unpadded slip | 15.6" Padded rear sleeve | 16" Suspended fleece-lined sleeve | 13.3" Padded internal divider |
| Wet/Dry Pocket | Basic zippered pocket | Waterproof TPU lined pocket | Heat-sealed seamless TPU pocket | Water-resistant zippered pouch |
| Carry Options | Dual handles + Shoulder strap | Dual handles + Backpack harness | Dual handles + Ergo shoulder strap | Long tote handles + Crossbody |
3. Performance Textiles & Advanced Material Engineering
The exterior textile represents 40% to 55% of a gym bag's direct material cost and directly dictates its tactile hand-feel, structural drape, tear resistance, and lifespan.
3.1 Exterior Shell Fabrics: Polyester vs. Nylon vs. Technical Laminates
When engineering custom gym bags, sports brands must select materials based on physical performance parameters rather than visual appearance alone:
- 600D / 900D High-Density Polyester (The Industry Workhorse):
- Structure: Woven from tightly twisted polyester filaments with a dual-pass back polyurethane (PU) or thermoplastic elastomer (TPE) coating.
- Properties: Exceptional color-fastness against UV sunlight and heavy laundering; high structural dimensional stability; excellent cost efficiency.
- Best For: Mid-tier activewear collections, fitness chain promotional merchandise, and team sports equipment bags.
- 500D / 1000D High-Tenacity Cordura Nylon (The Extreme Durability Standard):
- Structure: Woven from air-textured high-tenacity nylon 6,6 filaments offering world-class tensile strength and abrasion resistance.
- Properties: Resists over 50,000 cycles on the Martindale abrasion test without fiber fraying; highly resistant to tearing even when punctured; superior military-grade tactile drape.
- Best For: Premium tactical fitness bags, CrossFit training duffels, and commercial outdoor athletic gear.
- TPU-Laminated Waterproof Ripstop (The High-Tech Weatherproof Choice):
- Structure: 420D to 840D polyester or nylon base fabric laminated with an exterior or interior matte Thermoplastic Polyurethane (TPU) membrane.
- Properties: 100% waterproof surface (water column rating > 10,000 mm H2O); easily wiped clean of gym chalk, mud, and liquid spills; modern technical aesthetic.
- Best For: Aquatic sports, outdoor obstacle course racing, and high-end futuristic activewear lines.
- GRS-Certified Recycled RPET Polyester (The Sustainable Solution):
- Structure: Manufactured by mechanically chopping, melting, and re-spinning post-consumer recycled plastic bottles into high-tenacity polyester yarn.
- Properties: Delivers 100% identical tensile strength, tear resistance, and dye-lot saturation as virgin polyester while reducing manufacturing carbon footprint by up to 45%. Fully verifiable via Global Recycled Standard (GRS) transaction certificates.
- Best For: Eco-conscious activewear brands, sustainable yoga studios, and corporate ESG-mandated merchandise programs.
| Fabric Grade & Code | Base Polymer Yarn | Denier / Yarn Spec | Fabric Weight (GSM) | Hydrostatic Water Head | Tensile Rupture Strength | Relative Cost Index |
|---|---|---|---|---|---|---|
| 600D Standard Poly | 100% Virgin Polyester | 600D × 600D / 64T | 220 – 240 g/m² | 1,000 mm (PU 1-Pass) | 850 N | 1.0x (Baseline) |
| 900D Matte Twisted Poly | 100% Virgin Polyester | 900D × 900D / 58T | 310 – 340 g/m² | 1,500 mm (PU 2-Pass) | 1,250 N | 1.35x |
| 1680D Ballistic Poly | 100% Virgin Polyester | 1680D 2-Ply Basketweave | 420 – 460 g/m² | 2,000 mm (PU 2-Pass) | 1,850 N | 1.75x |
| 500D Cordura Nylon | 100% High-Tenacity Nylon 6,6 | 500D × 500D Air-Textured | 240 – 260 g/m² | 1,500 mm (PU 2-Pass) | 1,600 N | 2.20x |
| 1000D Cordura Nylon | 100% High-Tenacity Nylon 6,6 | 1000D × 1000D Heavy Duty | 340 – 380 g/m² | 2,000 mm (PU 2-Pass) | 2,400 N | 2.85x |
| 420D TPU Matte Ripstop | Nylon Base + TPU Membrane | 420D Grid Reinforcement | 280 – 310 g/m² | 10,000 mm (Laminated) | 1,450 N | 2.40x |
| 600D GRS Recycled RPET | 100% Post-Consumer PET | 600D × 600D Recycled | 230 – 250 g/m² | 1,000 mm (Water-based PU) | 820 N | 1.25x |
3.2 Interior Linings & Antimicrobial Hygiene Coatings
The interior of a gym bag is subjected to constant biological exposure—damp sweat, athlete body oils, locker room humidity, and spilled nutritional powders. Using generic low-grade 190T polyester lining results in rapid odor retention and internal seam delamination.
- 210D / 420D High-Density PU Ripstop Lining: Provides smooth structural gliding when sliding shoes and apparel in and out, while resisting internal punctures from keys and sharp gym accessories.
- Silvadur™ / Sanitized® Silver-Ion Antimicrobial Finishes: Embedded silver-ion technology applied during fabric finishing inhibits the growth of odor-causing bacteria, mold, and mildew inside closed pockets.
- High-Contrast Hi-Viz Interior Colors: Utilizing bright interior lining fabrics (such as Safety Orange, Volt Green, or Warm Gold) rather than pitch black allows athletes to instantly locate small gym accessories (earbuds, lifting chalk, keys, locks) in dimly lit locker rooms and workout studios.
3.3 Micro-Coating Chemistry: PU vs. PVC vs. TPE vs. Silicone
The backing coating applied to the reverse side of the exterior textile determines its waterproofing lifespan, flexibility in cold winter conditions, and regulatory compliance status:
- Polyurethane (PU) Coatings: The premier commercial standard for athletic bags. Lightweight, highly flexible, odorless, and fully compliant with all global environmental mandates (CPSIA, Prop 65, REACH). Applied in 1-pass (400–600 mm), 2-pass (1,000–1,500 mm), or 3-pass (2,000+ mm) layers.
- Thermoplastic Elastomer (TPE) Backing: A non-toxic, eco-friendly rubberized laminate that replaces toxic PVC. Offers exceptional structural body and crisp shape retention, preventing bags from collapsing into limp fabric puddles when empty.
- Polyvinyl Chloride (PVC) Backing (Deprecated for Premium Brands): Traditional heavy rubberized coating. While inexpensive, standard PVC adds substantial dead weight, cracks in sub-zero winter temperatures, and frequently fails international phthalate chemical testing unless expensive eco-plasticizers are specified.
- C0 PFAS-Free Durable Water Repellent (DWR) Surface Finish: Applied to the face of the fabric to create a lotus-leaf water beading effect. Senszx utilizes modern fluorine-free C0 chemistry, achieving Grade 90+ spray ratings (AATCC 22) without hazardous forever chemicals.
4. Specialized Functional Compartment Engineering
What distinguishes a purpose-built athletic gym bag from a generic travel duffel is the meticulous engineering of specialized functional compartments designed around the athlete's daily training routine.
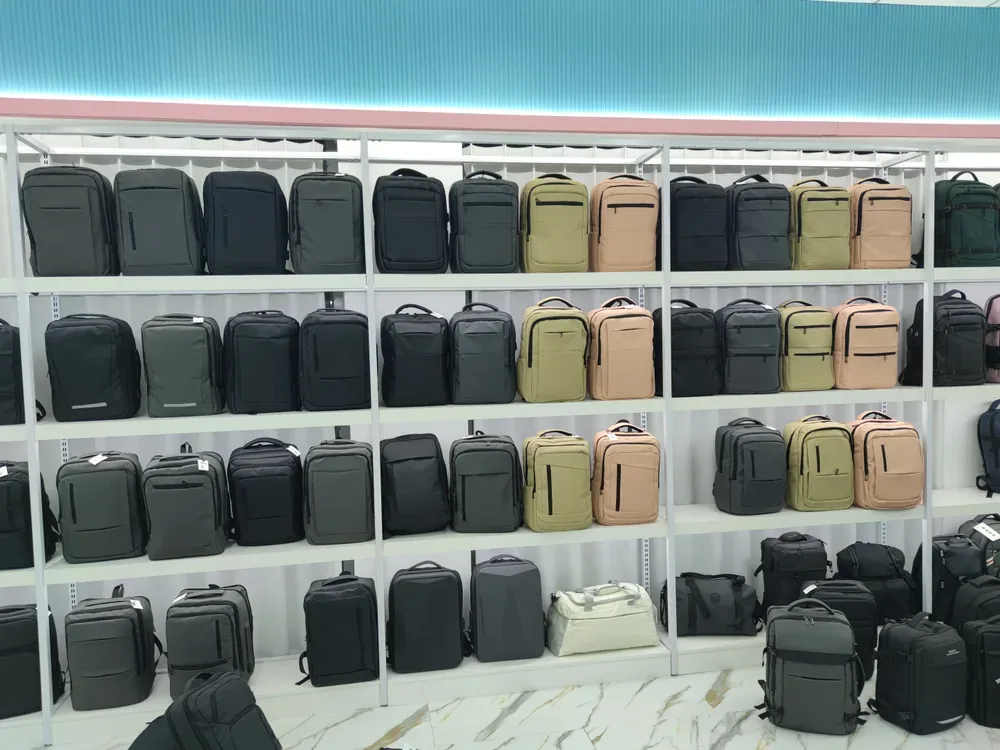
4.1 The Expandable Ventilated Shoe Tunnel
Footwear is the heaviest, dirtiest, and bulkiest item carried in a sports bag. A poorly designed shoe pocket steals fixed volume from the main cavity even when empty, or collapses under the weight of clean clothes.
- Collapsible Elastic Tunnel Construction: Engineered using flexible 210D PU-coated ripstop or washable TPU that lays completely flat against the interior sidewall when shoes are not carried, preserving 100% of the main cavity volume.
- Dual Laser-Cut Ventilation Grommets: Two to four precision laser-cut brass or zinc eyelets with breathable interior mesh screens installed on the exterior end-cap panel allow continuous passive airflow, venting moist air and preventing fungal spore buildup.
- Extended Longitudinal Depth: Sized to a minimum length of 36 cm (14.2 inches) to comfortably fit oversized high-top basketball shoes, cross-training lifting shoes with rigid heel cups, or muddy trail running cleats up to US Men's size 14 without crushing the upper collar.
4.2 Seamless Heat-Sealed Wet/Dry Separation Compartments
Athletes routinely need to store sweat-drenched compression apparel, post-workout towels, or damp swimsuits without allowing moisture to bleed through internal stitching into the main dry chamber.
| Wet/Dry Barrier Engineering Layer | Raw Material Construction | Fabrication Technology | Functional Barrier Role |
|---|---|---|---|
| 1. Dry Main Cavity Lining | 210D High-Density Poly Ripstop | Precision Single-Needle Lockstitch | Clean apparel, electronic devices, dry towel storage |
| 2. Heat-Sealed Wet Membrane | 0.15 mm Non-Porous Matte TPU | High-Frequency Ultrasonic Heat Welding | 100% leakproof sweat and biological moisture containment |
| 3. Exterior Shell Substrate | 600D / 900D DWR-Coated Polyester | Computerized Double-Needle Seaming | Abrasive protection, weatherproofing, color aesthetics |
- Ultrasonic / High-Frequency Welded Seams: Conventional needle stitching creates thousands of microscopic puncture holes through which liquid sweat and moisture seep over time. High-performance wet pockets utilize high-frequency welded 0.15 mm TPU membranes that eliminate all needle perforations, creating an impenetrable waterproof basin.
- Water-Resistant Reverse PU Zippers: Finished with a polyurethane-coated reverse coil zipper tape that prevents liquid from escaping through the zipper teeth when the bag is tossed horizontally into a car trunk or locker.
4.3 Thermal Insulated Hydration & Shaker Sleeves
Keeping pre-workout drinks cold and preventing protein shaker bottles from sweating condensation over clean gym apparel is a major value-add for athletic customers.
- PEVA Food-Grade Insulation: Lined with 4 mm closed-cell EPE thermal foam encased in seamless, BPA-free PEVA silver foil lining that maintains internal bottle temperatures for 4 to 6 hours while allowing effortless sanitization.
- Elastic Expansion Gussets: External side bottle holders feature engineered Lycra or 4-way stretch mesh bellows with an internal silicone grip ring, securely holding wide-mouth 32 oz (1,000 ml) stainless steel bottles or blender shakers without slipping out during rapid walking.
4.4 Sport-Specific Modular Engineering: CrossFit, Martial Arts, Aquatic & Racquet Sports
Depending on your brand's specific athletic niche, Senszx engineers specialized modular hardware and pocket architectures:
| Athletic Training Discipline | Primary Specialized Gear Carried | Custom Engineering Solution & Hardware |
|---|---|---|
| Functional Fitness & CrossFit | Heavy 4-inch leather weightlifting belts, knee sleeves, wrist wraps, lifting chalk | External dual quick-release buckle webbing straps to cradle lifting belts externally; chalk-proof wipeable pocket |
| Boxing & Martial Arts (MMA) | 16 oz boxing gloves, shin guards, hand wraps, mouthguards | Dual oversized breathable mesh side-vent chambers allowing airflow to dry damp boxing gloves rapidly |
| Swimming & Triathlon | Wet wetsuits, swim goggles, kickboards, pool towels | Full-length waterproof roll-top wet dry bag liner with drainage eyelets and anti-fog goggle microfleece sleeve |
| Racquet & Paddle Sports | Tennis racquets, pickleball paddles, ball cans | Padded diagonal exterior racquet sleeve with auto-locking zipper slider to hold handles firmly in place |
| Urban Bike & Run Commuters | Laptop, cycling helmet, LED safety lights, U-lock | Exterior deployable stretch helmet net, 3M reflective loop anchor, padded rear laptop suspended sleeve |
5. Structural Hardware, Webbing & Heavy-Duty Ergonomics
A gym bag's lifespan is defined by its weakest load-bearing junction. When an athlete carries 20 kg of iron weights, kettlebells, and gear, massive shear and tensile forces concentrate on the shoulder strap buckles, handle anchor patches, and zipper terminal stops.
| Structural Component | Material Specification | Minimum Tensile Break Strength | Engineering Construction Standard |
|---|---|---|---|
| Main Hand Grips Webbing | Seatbelt-Grade High-Tenacity Nylon | > 1,500 kg (15 kN) | Continuous wrap underneath base panel with double Box-X reinforcement stitching |
| Shoulder Strap Swivel Hooks | Die-Cast Zinc Alloy or Anodized Alum | > 120 kg (1.2 kN) | 360-degree rotation swivel to prevent strap twisting; electroplated matte black finish |
| Main Cavity Zippers | #8 or #10 Heavy-Duty Reverse Coil | > 120 N Lateral Pull | Double metal sliders with ergonomic molded silicone pullers and dual padlock loops |
| Side & Pocket Zippers | #5 Water-Resistant Reverse Coil | > 80 N Lateral Pull | PU-laminated zipper tape with TPU injection sealed terminal zipper garages |
| Strap Adjustment Sliders | Virgin Polyoxymethylene (POM / Acetal) | > 90 kg (0.9 kN) | High-impact freeze-resistant polymer, ribbed non-slip friction teeth |
| Shoulder Padding Core | Dual-Density EVA + Perforated PU Foam | 80 kg/m³ Density | 12 mm total thickness encased in 3D breathable air mesh with bound seams |
| Structural Stress Zone | Standard Commercial Construction Failure | Senszx Heavy-Duty Industrial Engineering Standard |
|---|---|---|
| Top Handle Anchor | Single seam stitched into edge binding (Tears at 12–15 kg) | Internal 600D backer plate + 40×50mm Box-X + Dual 42-stitch bar-tacks (>45 kg payload) |
| Base Panel Corners | Unreinforced single-ply polyester (Wears through in 3 months) | Dual-layer 1680D Ballistic base + 2mm high-density EVA foam + Molded rubber riser feet |
| Shoulder Strap Buckle | Recycled brittle plastic (Cracks under sub-zero winter temperatures) | Virgin POM Acetal hardware tested to -20°C cold drop impact (>90 kg break threshold) |
| Main Zipper Seams | Single lockstitch with loose thread ends | Double-stitched high-tensile nylon thread with bound seam tape and bartacked terminal stops |
5.1 The Science of Handle Anchor Reinforcement
At Senszx, we never stitch handle webbing directly into the top edge binding seam alone. When loaded with 20 kg, a single-seam handle anchor will tear out along the needle perforation line within weeks.
Instead, our production lines execute an industrial Three-Layer Reinforced Anchor Protocol:
- Internal Hypalon / 600D High-Tear Backer Plate: A 50 mm × 60 mm high-density reinforcing patch is inserted on the reverse side of the shell fabric before sewing.
- Double Perimeter Lockstitch + Box-X Geometry: The heavy-duty nylon webbing is sewn through both the shell and backer using bonded high-tensile nylon thread #40 (V-69) at a precise density of 7 to 8 stitches per inch (SPI).
- Dual High-Density Bar-Tack Headers: A computerized bar-tack machine applies two 42-stitch high-density reinforcing bars across the top and bottom stress edges of the Box-X, distributing dynamic lifting shocks across the entire panel plane.
5.2 Sewing Thread Chemistry: Bonded Nylon vs. Spun Polyester
Many low-cost factories use standard spun polyester garment thread in bag assembly. Under dynamic kinetic jerking and heavy friction, spun polyester fibers heat up, fray, and shear.
Senszx exclusively specifies Continuous Filament Bonded Nylon Thread (Grade V-69 / #40 or V-92 / #20) for all critical structural seams:
- Bonding Treatment: The multi-ply nylon filaments are coated with a specialized polymeric bonding agent that prevents untwisting, ply separation, and friction heating inside high-speed industrial sewing needles (3,000 RPM).
- Tensile Break Threshold: A single V-69 bonded nylon stitch thread withstands 4.8 kg (47 N) of direct tensile pull, compared to only 1.8 kg for generic spun polyester thread, ensuring total seam integrity under extreme loads.
6. Custom Branding, Logo Embellishment & Aesthetics
A sports brand's logo embellishment must withstand heavy physical abrasion, sweat exposure, rain, and frequent cleaning without cracking, peeling, or fading.
6.1 Comparing Logo Branding Techniques for Athletic Bags
| Branding Technique | Visual & Tactile Aesthetic | Durability & Water Resistance | Minimum Line Detail Precision | Tooling / Setup Cost | Ideal Application |
|---|---|---|---|---|---|
| 3D Molded Silicone Patch | Modern, matte rubberized tactile relief, multi-level 3D depth | 100% Waterproof, Zero Fading, highly abrasion-resistant | 0.3 mm ultra-sharp lines | $80 – $150 (Molded Steel Tooling) | Main front logo emblem, side shoulder pad branding |
| High-Density Screen Print | Clean athletic finish, slightly raised ink profile (0.5 mm) | High flexibility, resistant to cracking under flexing | 0.5 mm line width | $25 – $40 per color screen | Large side-panel brand wordmarks, oversized graphics |
| 3M™ Reflective Heat Transfer | Sleek silver/iridescent finish that glows brilliantly under light | High reflectivity, water-resistant; avoids high-temp dryer | 0.4 mm line width | $30 – $50 laser cutting die | Night-running safety logos, technical brand accents |
| High-Density Embroidery | Classic heritage athletic feel, rich thread luster | Virtually indestructible, immune to abrasion and weather | 0.8 mm (limited on tiny text) | $20 – $35 digital tape punch | Heritage sports club crests, collegiate team patches |
| Custom Molded Zinc Pullers | Matte-black or gunmetal electroplated solid alloy zipper pulls | Lifetime durability, premium weighted luxury hand-feel | 0.2 mm debossed/embossed | $90 – $180 zinc alloy injection mold | Main cavity zipper sliders, pocket pullers |
| Custom Jacquard Webbing | Logo or brand slogan woven directly into the continuous webbing | 100% permanent, zero surface ink, completely snag-free | Woven pixel resolution | $120 – $200 loom programming setup | Continuous shoulder straps, top carry handles |
6.2 Designing a Cohesive Athletic Bag Colorway Collection
Commercial sports brands rarely launch a single bag in black alone. A well-planned colorway collection creates visual impact across e-commerce storefronts and retail displays:
- The Core Anchor Neutral (50% – 60% of Production Volume): Matte Onyx Black, Shadow Grey, or Deep Midnight Navy. Anchors volume, guarantees steady sell-through, and fits conservative gym-to-office commuters.
- The Seasonal Trend / Heritage Tone (25% – 30% of Volume): Olive Drab, Sage Green, Desert Sand, or Rust Terracotta. Drives editorial lifestyle marketing, social media lookbooks, and seasonal product drops.
- The High-Energy Accent / Limited Edition (10% – 15% of Volume): Neon Lime, Safety Volt, Hyper Crimson, or Iridescent Reflective. Generates influencer excitement, visual contrast in digital ads, and collector demand.
7. Quality Assurance, Compliance Testing & International Standards
In the European Union, North America, Australia, and the Middle East, commercial sports goods are subject to stringent chemical safety and physical durability regulations. Failing an import customs random test can result in total shipment impoundment and catastrophic product recalls.
7.1 Laboratory Chemical Compliance Framework
Senszx verifies all raw textiles, coatings, foam cores, zippers, and hardware through certified third-party testing laboratories (SGS, TÜV, Intertek) to ensure full compliance with global consumer safety regulations:
- US CPSIA (Consumer Product Safety Improvement Act): Zero hazardous lead content in surface coatings and substrates (< 90 ppm); total phthalates (< 1,000 ppm).
- California Proposition 65: Strict compliance with permissible limits for phthalates (DEHP, DBP, BBP, DINP, DIDP, DNHP) and heavy metal leachability.
- EU REACH Regulation (EC No. 1907/2006): Complete verification against the SVHC (Substances of Very High Concern) candidate list, ensuring zero azo dyes, nickel release on metal hardware, or carcinogenic polycyclic aromatic hydrocarbons (PAHs).
- PFAS-Free Water Repellency: In compliance with recent US state and EU environmental directives, Senszx utilizes eco-friendly C0 (zero fluorine) Durable Water Repellent (DWR) formulations, delivering exceptional water-beading performance without persistent fluorinated chemicals.
7.2 Physical Mechanical Stress Testing Protocols
Before mass packaging, pre-production master prototypes and bulk sampling lots undergo exhaustive mechanical stress testing at our Baigou quality laboratory:
| Physical Stress Test Protocol | Applied Mechanical Parameter | Industry Standard Passing Threshold | Senszx Verified Quality Baseline |
|---|---|---|---|
| Dynamic Jerk Oscillating Drop | 30 kg internal payload / 1.2 m drop height | 1,000 continuous drops without seam rupture | 1,500 continuous cycles (Zero seam failure) |
| Seam Tensile Rupture Pull | Constant velocity 300 mm/min | > 350 N minimum rupture resistance | > 450 N high-tensile resistance |
| Zipper Lateral Burst Pull | Transverse tensile stress on closed teeth | > 120 N pull force | > 160 N heavy-duty burst threshold |
| Martindale Fabric Abrasion | 12 kPa continuous pressure load | > 35,000 cycles without yarn fraying | > 50,000 cycles (Cordura / Ballistic poly) |
| Cold Impact Buckle Drop | -15°C cold chamber / 2.5 kg drop hammer | Zero polymer cracking or fracture | 100% Virgin POM Acetal compliance |
| 100% Metal Needle Detection | Dual-head automated conveyor sensor | Zero ferrous metal fragments (> 0.8 mm) | 100% unit-level automated scanning |
8. The Senszx OEM/ODM Manufacturing Workflow
Sourcing custom gym bags from an experienced OEM/ODM manufacturer should follow a predictable, transparent engineering roadmap from initial concept discussion to final container loading.
| Production Workflow Stage | Core Manufacturing Activities & Deliverables | Timeline Duration | Primary Quality Gate & Milestone |
|---|---|---|---|
| Stage 1: Tech Review & BOM Costing | Tech pack intake, dimensional CAD drafting, fabric yield calculation, itemized FOB quotation | 24 – 48 Hours | Formal engineering BOM sign-off |
| Stage 2: Master Pattern Prototyping | 2D CAD pattern digitization, automated laser cutting of sample panels, master sample assembly | 3 – 5 Business Days | Physical prototype dispatch for fit review |
| Stage 3: Lab-Dips & Pre-Production (PPS) | Pantone lab-dip color strike-offs, custom hardware tooling review, golden seal PPS assembly | 5 – 7 Calendar Days | Signed pre-production golden seal sample |
| Stage 4: Automated Cutting & Sewing | Multi-ply tension-free spreading, vacuum CNC cutting, modular parallel sewing lines, in-line QC | 20 Calendar Days (500–5,000 units) | In-process AQL 1.5 statistical QC inspection |
| Stage 5: 100% Final QC & Global Export | 100% thread trimming, zipper lubrication test, metal needle detection, barcoded cartoning | 2 – 3 Days | Final customs export clearance & loading |
Stage 1: Technical Consultation & Target Cost Engineering (24–48 Hours)
Our senior engineering team reviews your design files, reference photos, or CAD tech pack. We conduct a detailed Bill of Materials (BOM) analysis, identify potential structural failure points, recommend optimized fabric yields, and issue a transparent, itemized FOB quotation based on your target order volume tiers.
Stage 2: Rapid Pattern Engineering & Master Sample Prototyping (3–5 Days)
Our specialized master sample room utilizes automated CAD pattern-making software and high-precision laser cutters to construct physical master prototypes. We verify silhouette balance, zipper smoothness, pocket ergonomics, and load distribution, dispatching high-resolution photo/video reviews and express courier samples directly to your design studio.
Stage 3: Lab-Dip Approvals & Pre-Production Sample (PPS) Sign-Off (5–7 Days)
We produce customized Pantone-matched textile lab dips, verify custom molded hardware tooling, and assemble the final Pre-Production Sample (PPS). Once the golden seal sample is signed off by your procurement team, physical counter-specifications are permanently locked for mass manufacturing.
Stage 4: Automated Laser/CNC Cutting & In-Line Sewing Assembly (20 Calendar Days)
Bulk fabric rolls undergo automated multi-ply tension-free spreading and computer-guided vacuum CNC cutting. Cut panel bundles move into dedicated modular sewing lines where specialized single-needle lockstitch, double-needle edge binding, and computerized bar-tack workstations assemble the bags in parallel.
Stage 5: 100% Quality Inspection, Metal Needle Detection & Global Export
Every completed gym bag passes through our final quality gate: 100% manual thread trimming, zipper track lubrication testing, seam tension verification, and dual-head automated metal needle detection scanning. Bags are individually bagged in 0.05 mm LDPE polybags with printed suffocation warnings, barcoded, packed into 5-ply double-wall export master cartons, and palletized for global maritime container shipment.
8.1 The Pre-Production Golden Sample Verification Checklist
Before bulk fabric cutting begins on any commercial order, Senszx and the brand client execute a standardized 10-point Pre-Production Sample (PPS) verification checklist:
| Quality Inspection Parameter | Verification Standard & Tolerance Limit | Inspection Methodology |
|---|---|---|
| 1. Exterior Dimensions & Volume | Length, width, and height within ± 5 mm tolerance of CAD spec | Calibrated steel rule & 3D liquid/bead volume displacement |
| 2. Fabric Denier, Backing & GSM | Exact GSM weight, weave density, and PU coating thickness | Electronic micro-balance cut swatch & digital micrometer gauge |
| 3. Color Harmony (D65 Lightbox) | Delta E < 0.8 compared to approved physical Pantone swatch | Spectrophotometer & D65 standard commercial daylight cabinet |
| 4. Seam Stitch Density (SPI) | 7 to 8 stitches per inch uniformly across all structural seams | Optical stitch gauge magnifier inspection |
| 5. Zipper Glide & Terminal Stops | Smooth, snag-free track glide under 5 N force; sealed garages | 50 consecutive manual open/close cycles on closed bag |
| 6. Shoe Tunnel Expansion & Vents | Expands smoothly to 36 cm depth; breathable eyelets clear | Test fit with US Men's Size 14 cross-training shoe pair |
| 7. Wet Pocket Waterproof Seal | 100% watertight under 500 ml liquid water test (24 hours) | Submersion moisture barrier test (Zero seam leakage) |
| 8. Handle Anchor Pull Strength | Zero thread rupture or fabric distortion under 35 kg static load | Digital hanging crane scale tensile hold test (5 minutes) |
| 9. Hardware Finish & Swivel Action | Smooth 360° swivel rotation; scratch-resistant electroplating | Salt spray corrosion resistance testing (48 hours ASTM B117) |
| 10. Retail Barcodes & Packaging | Scannable GS1-128 / FNSKU barcode labels; warning prints | Handheld optical laser barcode scanner read verification |
9. Commercial Sourcing Parameters, MOQ Tiering & Unit Economics
Understanding the commercial cost structures and quantity tier economics of custom gym bag manufacturing allows brand directors to maximize gross profit margins while maintaining inventory agility.
9.1 Single-Track Custom OEM/ODM MOQ: 500 Pieces per Style
Senszx operates on a clear, single-track minimum order quantity of 500 pieces per style/colourway.
- Why 500 Pieces? In industrial sewn-goods manufacturing, 500 units represents the minimum threshold required to optimize fabric roll cutting yields (minimizing expensive textile scrap), amortize custom printing screen setups, and allow sewing line operators to achieve maximum Standard Allowed Minute (SAM) line-balancing efficiency.
- Pilot Development Fee Program for Emerging Brands: For high-growth athletic apparel startups and boutique fitness studio chains that require smaller initial market test runs, we provide a structured Development Fee Program. This covers comprehensive master pattern digitization, custom cutting die setups, and physical prototype iterations. When you subsequently issue your initial 500+ unit bulk mass production purchase order, 100% of the initial development fee is credited directly back against your bulk invoice.
9.2 Unit Cost Breakdown by Order Volume Tiers
The following table illustrates the typical FOB unit cost breakdown and margin expansion across standard manufacturing volume tiers for a premium, multi-compartment athletic gym duffel:
| Manufacturing Cost Component | 500 Units Tier (Base MOQ) | 1,000 Units Tier | 5,000 Units Tier | Key Scale & Efficiency Multiplier |
|---|---|---|---|---|
| Shell & Contrast Fabrics (600D/900D PU) | $3.85 | $3.40 | $2.95 | Direct mill roll purchasing & nested CNC cutting efficiency |
| Lining & Waterproof TPU Pockets | $1.45 | $1.25 | $1.05 | Bulk roll procurement of 210D ripstop & TPU membranes |
| Zippers, Sliders & Metal Hardware | $1.60 | $1.35 | $1.10 | Factory-direct bulk sourcing of #8 reverse-coil zippers |
| Nylon Webbing & High-Density Foam | $0.95 | $0.80 | $0.65 | Automated computerized webbing hot-cutting & bulk EVA foam |
| Custom Molded Silicone Logo Badge | $0.65 (Amortized Tooling) | $0.40 | $0.20 | Fixed steel injection mold cost amortized over volume |
| Direct Cut-and-Sew Labor (SAM/SAH) | $2.40 | $2.05 | $1.65 | Operator workstation muscle memory & line-balancing flow |
| Packaging & Master Export Cartons | $0.50 | $0.45 | $0.35 | Bulk 5-ply corrugated carton and LDPE polybag pricing |
| Total Estimated FOB Unit Price | $11.40 | $9.70 (-15%) | $7.95 (-30%) | Significant unit margin expansion at scale |
| Recommended Target Retail MSRP | $68.00 – $88.00 | $68.00 – $88.00 | $68.00 – $88.00 | Gross Profit Margin: 83% to 90% |
10. Frequently Asked Questions (FAQ) for Sports Brand Procurement Directors
Q1: Can Senszx develop custom gym bags based only on design sketches or reference photos?
Yes. While a finalized CAD technical pack accelerates timeline execution, our master pattern room frequently engineers full custom gym bags from dimensioned hand sketches, mood board concept images, or physical benchmark samples. During technical intake, we translate your aesthetic concepts into precise 2D pattern markers, recommend appropriate fabric deniers, and generate complete Bill of Materials (BOM) specifications for your approval.
Q2: How do we prevent sweat and moisture from leaking out of the wet laundry pocket?
We construct wet laundry pockets using seamless 0.15 mm Thermoplastic Polyurethane (TPU) or heavy-duty PEVA membranes bonded via high-frequency ultrasonic heat welding. Unlike conventional sewn seams that create needle puncture perforations, heat-sealed TPU creates a 100% leakproof, impermeable moisture barrier. Combined with a reverse-coil water-resistant zipper, wet towels and sweat-soaked compression wear remain completely isolated from clean clothes and electronics.
Q3: What is the optimal fabric denier for a lightweight yet tear-resistant gym duffel?
For the ideal balance of lightweight agility and rugged durability, we recommend 600D to 900D high-density polyester with dual-pass PU coating (fabric weight: 240 to 320 g/m²), or 500D high-tenacity Cordura nylon. These specifications deliver exceptional tear resistance (> 1,200 N tensile strength) while keeping the empty duffel weight between 650 g and 950 g, preventing athlete shoulder fatigue.
Q4: How are custom brand logos applied to high-stress areas of the bag?
For main exterior panels subjected to friction and flexing, we recommend 3D molded silicone rubber patches (sewn directly to the shell panel with perimeter groove stitching) or high-density silkscreen printing with flexible polyurethane binders. For subtle, high-end branding, we engineer custom debossed/embossed matte-black zinc alloy zipper pullers and jacquard woven logo webbing for continuous shoulder straps.
Q5: Can we customize interior pockets specifically for fitness tech accessories?
Yes. We frequently engineer custom padded interior compartments tailored to modern fitness technology, including fleece-lined suspended sleeves for 15.6"/16" laptops, shock-absorbing EVA foam pockets for electronic recovery massage guns, dedicated mesh sleeves for wireless heart-rate monitor straps, and soft-touch micro-fleece zip pockets for smartwatches and wireless earbuds.
Q6: What Incoterms do you offer, and can you deliver directly to Amazon FBA or 3PL warehouses?
We support standard international trade terms including FOB Tianjin / FOB Shanghai (for brands utilizing their own freight forwarders), CIF (destination port delivery), and full Door-to-Door DDP (Delivered Duty Paid). Under DDP terms, Senszx handles all export documentation, ocean container shipping, customs clearance, import tariff settlement, and final palletized trucking directly to Amazon FBA fulfillment centers or private 3PL distribution warehouses across the United States, Europe, Australia, and the Middle East.
Q7: How does Senszx ensure color accuracy across different fabric components and webbing?
We utilize the international Pantone Matching System (PMS / TCX) for all custom color formulations. During the pre-production phase, we produce physical textile lab dips and webbing swatch strike-offs under standard D65 commercial lightboxes for your team's visual and spectrophotometer sign-off, ensuring seamless color harmony across shell fabrics, lining, webbing, zippers, and trims.
Q8: What social compliance and ethical factory audit standards does Senszx maintain?
Senszx is fully audited and certified under BSCI (Business Social Compliance Initiative), ISO 9001 (Quality Management Systems), ISO 14001 (Environmental Management), and ISO 45001 (Occupational Health & Safety). We enforce strict ethical labor policies, fair living wages, comprehensive worker safety equipment, clean air-conditioned facilities, and zero child or forced labor, ensuring your brand maintains total ESG supply chain integrity.
Q9: Can you manufacture sustainable gym bags using recycled ocean or plastic bottle materials?
Yes. We maintain direct partnerships with certified GRS (Global Recycled Standard) yarn spinning mills. We can produce your entire custom gym bag collection using 100% GRS-certified Recycled RPET polyester or recycled nylon, complete with official Transaction Certificates (TC) that legally validate your brand's sustainability marketing claims.
Q10: How do we initiate a custom gym bag development project with Senszx?
To begin a project, submit your preliminary technical pack, reference sketches, or sample brief to our engineering team at [email protected] or connect via WhatsApp at +86 17331531825. Include your target order volume, desired functional features (shoe tunnel, wet pocket, laptop sleeve), target retail price tier, and timeline requirements. Our technical sales engineers will deliver a detailed BOM analysis, optimization recommendations, and an itemized quotation within 24 to 48 hours.
11. Summary: Partnering with a Specialized Athletic Bag OEM Manufacturer
In the competitive modern fitness and athletic apparel landscape, your product packaging and carry-all gear must reflect the exact same uncompromising quality, innovation, and performance as your core activewear garments.
By partnering with an experienced, vertically integrated OEM/ODM manufacturing specialist like Senszx, sports brands eliminate the costly trial-and-error, quality defects, and supply chain delays that plague unvetted suppliers. From automated CAD pattern engineering and precision CNC cutting to ultrasonic wet/dry compartment welding and rigorous 100% in-line quality validation, we transform your athletic gear vision into high-margin commercial reality.
Ready to Develop Your Brand's Custom Gym Bag Collection?
Contact our technical engineering and sourcing team today to review your design concepts, request physical master material swatches, or receive an itemized factory-direct quotation:
- Official Contact Email: [email protected]
- Direct Engineering Line / WhatsApp: +86 17331531825
- Manufacturing Campus Location: Baigou Industrial Luggage & Backpack Zone, Baoding, Hebei, China
- Explore Sourcing Guides & Catalogs:
- How to Write a Professional Custom Backpack Tech Pack
- How to Prepare an Accurate Custom Bag RFQ
- Comprehensive Custom Backpack Cost Breakdown & Pricing Tiers
- Senszx OEM/ODM Custom Backpack Manufacturing Services
- Custom Technical Fabric Selection & Denier Specifications
- Bespoke Zipper Pullers, Hardware & Buckle Directory
- Types of Backpacks: The Complete B2B Sourcing & Category Guide
- Senszx Factory Social Compliance & International Certifications
Hi, I'm Senszx Bag Manufacturer, Hope You Like This Blog Post.
With more than 20 years of experience in OEM/ODM/Custom luggage and bag, I'd love to share with you the valuable knowledge related to luggage and bag products from a top-tier Chinese supplier's perspective.
Senszx Factory
Est. 2006 · Baigou, China
Related articles
How to Choose the Right Materials for Travel Bags: The Complete Manufacturer Guide
A comprehensive B2B engineering guide to selecting travel bag materials: comparing polyester, nylon, Oxford, canvas, TPU coatings, hardware, and structural interlinings across durability, GSM, abrasion, and manufacturing cost.
Bulk Backpacks: The Complete Wholesale Buying Guide for 2027
How brands, distributors, schools and charities buy backpacks in bulk: sourcing paths, styles, fabrics, customization, unit price drivers, MOQ, lead times, QC and shipping.
Wholesale Toiletry Bags: The Complete Sourcing Guide for 2027
How travel brands, grooming labels, retailers and distributors source toiletry bags in bulk: styles, materials, customization, MOQ, pricing, QC and shipping.
Get a Custom Bag Quote from Our China Factory
Our sales team is online around the clock and usually replies within the hour.
Email
[email protected]Factory
Qinzheng Road No.89, New Industry Zone, Baigou Town
Baoding City, Hebei Province 074004, China