Sports Bag Manufacturing with Shoe Compartments: The Complete B2B Guide to Gym Duffels, Ventilated Shoe Tunnels & Custom Athletic Bag OEM/ODM Production
The definitive B2B sourcing guide on sports bag manufacturing with shoe compartments. Master ventilated shoe tunnel engineering, waterproof wet/dry separation, 900D/1200D textile selection, 5,000-cycle jerk testing, single-track 500 MOQ economics, and DDP export logistics.
Sports Bag Manufacturing with Shoe Compartments: The Complete B2B Guide to Gym Duffels, Ventilated Shoe Tunnels & Custom Athletic Bag OEM/ODM Production
In the booming global activewear, fitness lifestyle, team sports, and boutique gym market, the sports duffel bag has evolved from a basic canvas gym sack into a sophisticated, multi-compartment personal performance system. Today’s fitness consumer leads an integrated, fast-paced life: transitioning seamlessly from an early morning CrossFit workout or hot yoga session to a corporate office workstation, followed by an evening flight or weekend tournament.
Throughout these dynamic transitions, the athlete faces a persistent hygiene and organization dilemma:
- Where do dirty, sweaty running shoes or muddy soccer cleats go without touching clean office shirts and laptops?
- How can soaking wet gym towels and sweaty activewear be stored without creating mold, bacterial growth, and foul odors inside the main compartment?
- How can a duffel maintain its sleek, structured aesthetic when fully packed with bulky athletic footwear?
The sports bag with an integrated shoe compartment solves these critical friction points. By isolating contaminated footwear in a dedicated, ventilated, wipe-clean tunnel while providing separate waterproof wet/dry cavities, insulated shaker bottle holders, and padded laptop compartments, it elevates the user experience from chaotic clutter to disciplined athletic readiness.
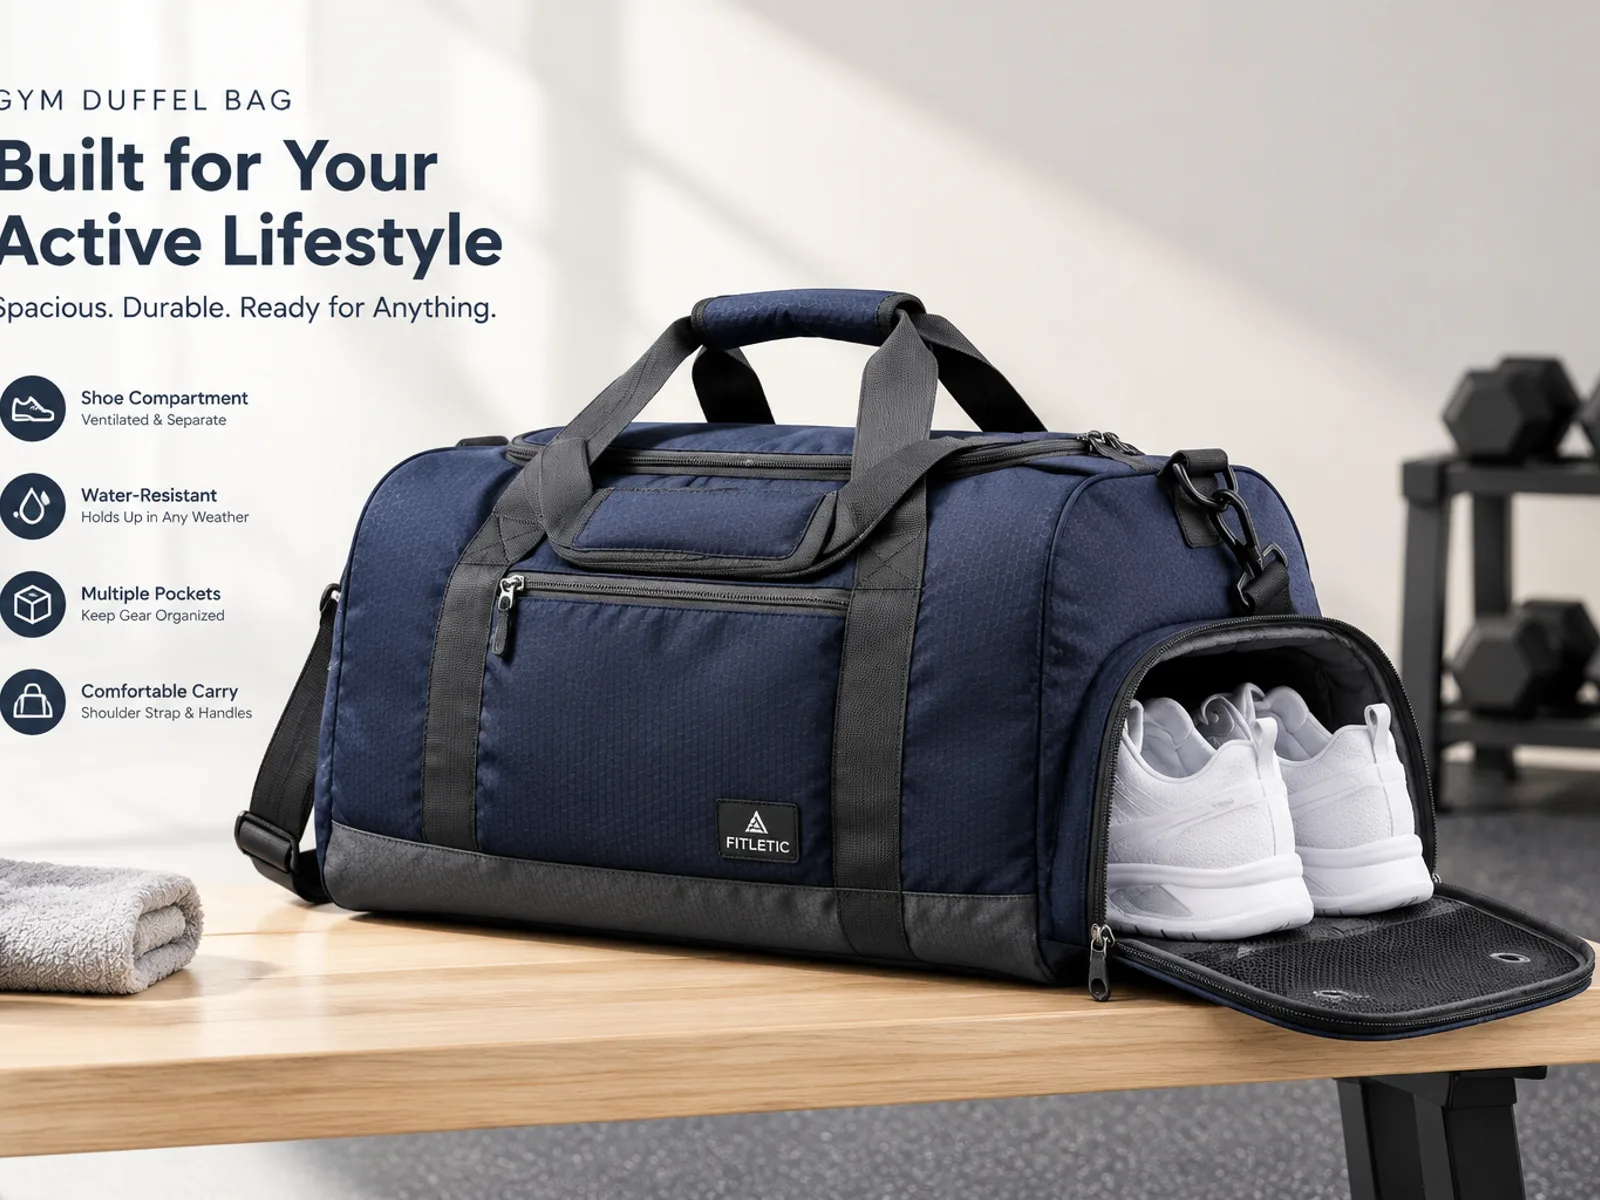
For global sportswear brands, fitness apparel labels, gym franchises, and private-label innovators, engineering a market-leading sports bag requires deep expertise in functional textile engineering, anti-microbial treatments, laser-cut ventilation mechanics, dynamic load-bearing handle construction, and high-volume mass production.
At Senszx, founded in 2006 in Baigou, China—the world’s premier industrial epicenter for bag and luggage manufacturing—we have spent over two decades engineering, prototyping, and scaling custom sports bags, gym duffels, and athletic gear carriers for leading global brands across North America, Europe, Australia, and worldwide markets. Operating 100 synchronized production sewing lines with BSCI, ISO 9001, ISO 14001, and ISO 45001 accreditations, we combine automated CNC cutting precision, master pattern room prototyping, single-track 500 MOQ flexibility, 3-5 day rapid sampling, and 20-day mass manufacturing turnaround.
This comprehensive B2B sourcing guide deconstructs every layer of sports bag engineering, shoe compartment architecture, wet/dry separation technology, material selection, quality control protocols, and procurement economics.
1. The Modern Athletic Market: Why Dedicated Shoe Compartments Are Non-Negotiable
In modern sports soft goods, product functionality directly determines customer satisfaction and retail sell-through. An athletic bag without dedicated footwear isolation suffers high return rates and poor product reviews.
The Dual Storage Dilemma In Athletic Carry
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| CLEAN GEAR ZONE | Fresh apparel, work laptop, protein supplements, clean socks |
| CONTAMINATED ZONE | Sweaty running shoes, muddy cleats, damp towels, chalk-covered grips |
| SENSZX ENGINEERING SOLUTION | Hydrophobic, Ventilated, Anti-Microbial Floating Tunnel Barrier |
1.1 Hygiene, Bacteria & Odor Prevention
Athletic footwear after an intense training session generates heat, moisture, and bacteria (Brevibacterium and Staphylococcus). When shoes are placed in an unventilated, enclosed compartment:
- Trapped moisture accelerates bacterial reproduction, creating persistent foul odor.
- Sweat and dirt transfer to neighboring clean apparel and tech gear.
- In-line shoe tunnel engineering with breathable metal eyelets and silver-ion treated hydrophobic linings allows continuous passive air circulation, dissipating moisture vapor while isolating dirt.
1.2 Cross-Contamination Physics: Odor Molecular Diffusion & Microbial Colonization
When footwear is sealed in a standard non-isolated duffel bag:
- Volatile Organic Compounds (VOCs) and isovaleric acid molecules emitted from sweat-soaked shoe insoles permeate porous synthetic apparel fabrics within 30 minutes.
- Bacteria transfer readily to gym towels and clean garments.
- Senszx's sealed, polyurethane-coated floating nylon shoe barrier creates a physical and molecular barrier, completely arresting vapor and microbial cross-contamination.
1.3 Biomechanics of Unilateral Shoulder Carry vs. Dual-Strap Backpack Conversion
Carrying a heavy 15kg to 25kg sports duffel over one shoulder creates asymmetric cervical and lumbar spine compression:
- Unilateral Clavicle Pressure: Standard 38mm webbing straps generate acute contact pressures exceeding 45 kPa on the clavicle bone, causing muscle fatigue within 15 minutes.
- Hideaway Dual-Strap Backpack Conversion: Senszx crafts hybrid sports duffels equipped with concealed, contoured EVA backpack shoulder straps stowed inside a zippered back panel. The user can convert the duffel into an ergonomic backpack in under 5 seconds, distributing the payload symmetrically across both shoulders during subway commutes or airport transit.
2. The 5 Core Archetypes of Sports & Gym Bags with Shoe Storage
Sourcing teams must select the appropriate bag archetype based on the specific sport discipline, user journey, and volumetric capacity requirements:
The 5 Core Sports & Gym Bag Archetypes With Shoe Storage
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| ARCHETYPE 1 | THE CLASSIC BARREL DUFFEL] Vol: 25L - 35L Focus: Minimalist daily gym |
| ARCHETYPE 2 | THE TECHNICAL FITNESS DUFFLE] Vol: 35L - 50L Focus: Multi-sport & weekend |
| ARCHETYPE 3 | THE GYM-TO-OFFICE HYBRID BACKPACK]Vol: 28L - 38L Focus: Commuter with laptop |
| ARCHETYPE 4 | THE TEAM GEAR EXPEDITION DUFFEL] Vol: 60L - 95L Focus: Team sports & cleats |
| ARCHETYPE 5 | THE COMPACT ACTIVE CROSSBODY] Vol: 12L - 18L Focus: Yoga & light studio |
2.1 Detailed Archetype Breakdown and Engineering Specifications
| Sports Bag Archetype | Volumetric Range | Typical Dimensions (L x W x H) | Primary Structural Features | Target Customer & Usage Scene |
|---|---|---|---|---|
| 1. Classic Barrel Gym Duffel | 25L to 35L | 480 x 260 x 260 mm | Cylindrical profile, side-entry collapsible shoe tunnel, front quick-access pocket, 38mm seatbelt webbing handles. | Daily gym goers, fitness class attendees, yoga practitioners. |
| 2. Technical Fitness Duffle | 35L to 50L | 560 x 300 x 290 mm | Structured rectangular base, ventilated shoe tunnel, heat-sealed TPU wet pocket, insulated shaker sleeve, padded shoulder strap. | CrossFit athletes, bodybuilding enthusiasts, weekend active travel. |
| 3. Gym-to-Office Hybrid Backpack | 28L to 38L | 500 x 320 x 220 mm | Bottom-entry collapsible shoe compartment, suspended 16" laptop sleeve, vertical sternum strap, hideaway backpack harness. | Corporate professionals, urban bike commuters, tech workers. |
| 4. Team Gear Expedition Duffel | 60L to 95L | 720 x 380 x 360 mm | Heavy 1680D ballistic base, rigid dual-cleat shoe compartment, U-shaped top lid opening, daisy-chain webbing. | Football, hockey, soccer, baseball teams, tournament travel. |
| 5. Compact Studio Crossbody | 12L to 18L | 400 x 200 x 200 mm | Lightweight 420D ripstop or neoprene, slim side shoe sleeve, exterior yoga mat buckle straps. | Studio pilates, barre, boutique cycling classes. |
Explore our complete specialized guides on custom gym bags for sports brands, custom travel bags, and our dedicated gym bag manufacturing facility.
3. Shoe Compartment Architecture & Ventilation Dynamics: Inverted Tunnels vs. Rigid Basins
The mechanical design of the shoe compartment dictates whether the bag remains functional and aesthetically balanced under varying load conditions.
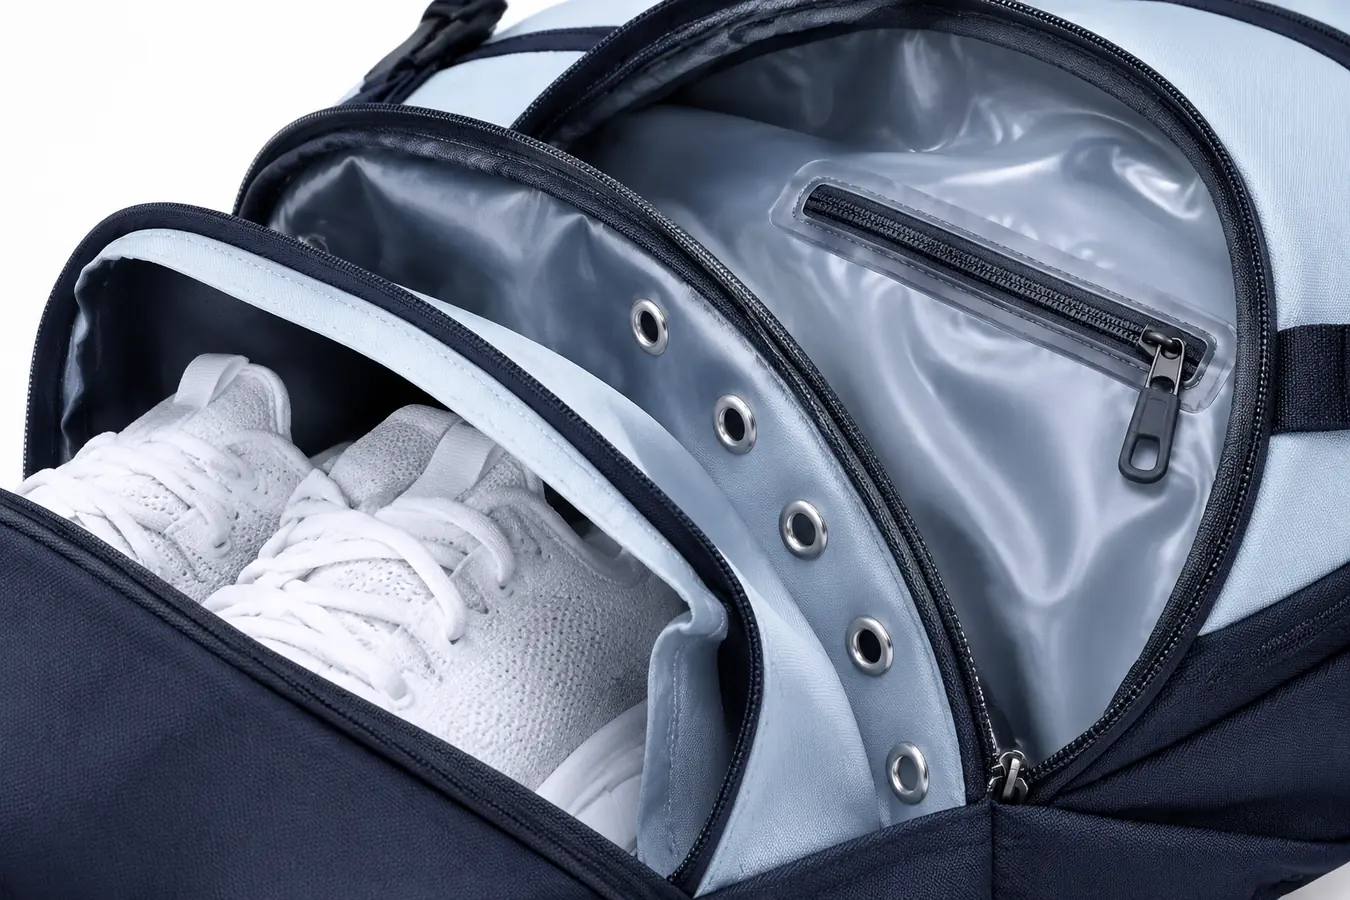
3.1 The Two Primary Shoe Compartment Engineering Configurations
The 2 Shoe Compartment Structural Configurations
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| CONFIG 1: COLLAPSIBLE INVERTED SHOE TUNNEL | Internal floating nylon sleeve, space adaptive |
| CONFIG 2: RIGID BOTTOM SEPARATION BASIN | Dedicated floor compartment, heavy cleats focus |
| Shoe Compartment Configuration | Spatial Mechanics | Engineering & Cost Advantages | Best Application in Sports Line |
|---|---|---|---|
| 1. Collapsible Inverted Shoe Tunnel | Space-Adaptive Floating Sleeve: Extends into the main duffel cavity when shoes are inserted; collapses 100% flat against side wall when empty. | Saves manufacturing weight; maximizes main compartment versatility; lower Bill of Materials cost. | Daily gym duffels, urban commuter backpacks, studio sports bags. |
| 2. Rigid Bottom Separation Basin | Fixed Perimeter Floor Compartment: Located beneath the main duffel floor with rigid 2.0mm HDPE frame sheet and dual zipper access. | Complete physical isolation; prevents heavy cleats or running shoes from pressing into upper apparel. | Large team sports gear bags, football/soccer duffels, multi-day travel. |
3.2 Ventilation Dynamics & Airflow Engineering
To ensure passive air circulation within the shoe tunnel:
- Dual Metal Ventilation Eyelets: Installing two 12mm laser-cut brass or aluminum grommets with matte black electroplating on the exterior side flap.
- Breathable Polyester Mesh Inserts: Integrating high-tensile 300g/m² micro-mesh panels along the upper seam of the shoe tunnel flap, promoting continuous chimney-effect airflow while preventing moisture buildup.
- Hydrophobic Wipe-Clean Linings: The interior of the shoe tunnel is constructed from 210D polyurethane-coated nylon that resists mud and dirt, allowing users to wipe the interior clean with a damp cloth in seconds.
3.3 Sizing Tolerances for Oversized Footwear (US Men's 14 / EU 48)
Standard consumer gym bags often restrict shoe compartments to US Men’s size 10. When an athlete wearing size 13 or 14 training shoes tries to pack their footwear, the tunnel jams, stressing zipper seams:
- Calibrated Volumetric Tunnel Length: Senszx engineers standard shoe tunnels with a 360mm length and 220mm height, effortlessly accommodating US Men’s size 14 high-top basketball shoes or heavy trail runners without distorting the duffel profile.
3.4 Heavy Cleat Puncture Protection: High-Density Polyethylene (HDPE) Base Liners
For sports team duffels (soccer, baseball, rugby, golf) carrying metal-spiked or hard-plastic molded cleats:
- Puncture-Proof Base Inserts: Lining the interior base of the shoe compartment with a die-cut 1.0mm HDPE sheet prevents sharp metal spikes from puncturing outer fabric seams or damaging floor surfaces when the bag is dropped.
3.5 Footwear Geometry Across Athletic Disciplines
Different sports impose radically distinct footwear dimensions and cleaning requirements:
- Running & CrossFit Trainers: Soft mesh uppers with wide soles requiring flexible tunnel expansion.
- High-Top Basketball Shoes: High ankle collars requiring vertical tunnel clearance (>180mm).
- Cycling Shoes with Look/SPD Cleats: Protruding plastic/carbon cleats requiring scratch-resistant tunnel linings.
- Ski & Snowboard Boots: Extra-heavy, rigid plastic boots requiring dedicated exterior bottom basins reinforced with 1680D ballistic nylon and drain grommets.
3.6 Wipe-Clean Chemical Stain Resistance
Shoe tunnels are exposed to turf mud, synthetic rubber black scuffs, and road grease. Senszx utilizes high-density 210D ripstop nylon with a multi-pass acrylic/polyurethane backing that resists chemical staining, allowing effortless sanitization with standard household disinfectant wipes.
3.7 In-Depth Shoe Tunnel CAD Pattern Geometry & Volume Displacement
When grading 2D CAD pattern cut files for collapsible shoe tunnels, Senszx engineers apply geometric volume displacement algorithms:
- Tapered Keystone Tunnel Drafting: Rather than sewing a flat rectangular sleeve, our pattern makers draft a trapezoidal keystone profile that is 20% wider at the inner heel termination than at the outer entry opening. This prevents footwear from binding against the side walls during insertion.
- Accordion Bellows Base Seams: Integrating inverted accordion pleats along the lower seam allows the floating sleeve to expand upward into unused upper duffel headroom rather than crushing lateral side pockets.
3.8 Heavy Z-Stitch & Double-Needle Seam Reinforcement
Because athletic shoes exert continuous forward and downward mechanical thrust when shoved into the tunnel, the perimeter join where the shoe tunnel meets the exterior duffel wall is reinforced with double-needle lockstitching and heavy 22mm herringbone binding tape, delivering a tensile seam burst strength exceeding 680 N.
4. Wet/Dry Separation Engineering: Heat-Sealed Waterproof TPU Liners
In addition to shoe storage, modern athletic duffels require dedicated Wet/Dry Separation Pockets to store sweaty compression shirts, damp swimsuits, and wet gym towels.
Wet/dry Separation Pocket Specification Matrix
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| WATERPROOF MEMBRANE] 0.20mm | 0.30mm Frosted or Transparent Thermoplastic Polyurethane (TPU) |
| SEAM WELDING TECHNOLOGY] High-Frequency Ultrasonic Thermal Welding (100% Hermetic Seal) | - |
| ZIPPER INTEGRATION] #5 Reverse Coil Zipper with PU Water-Resistant Coating Lamination | - |
| HYDROSTATIC BARRIER] Certified >10,000mm H2O Pressure Resistance (Zero Moisture Bleed) | - |
4.1 Ultrasonic Thermal Welding vs. Stitched Seams
Standard stitched seams create thousands of needle perforations through which moisture easily leaks into adjacent clean compartments. Senszx utilizes high-frequency ultrasonic thermal welding to bond the TPU wet pocket seams, creating a continuous, seamless hermetic barrier that completely prevents moisture migration even when carrying soaking wet swimwear.
4.2 Thermoplastic Polyurethane (TPU) vs. Low-Grade PVC
- Eco-Friendly TPU Membrane: 100% recyclable, completely free from toxic plasticizers and phthalates (100% CPSIA, REACH SVHC, and Cal Prop 65 compliant), remains supple and crack-resistant down to -30°C, and exhibits high hydrolysis resistance against laundry detergents and chlorinated pool water.
- Why PVC is Prohibited: Traditional PVC liners release volatile chemical odors, stiffen in cold temperatures, and frequently fail US Customs chemical audits.
4.3 Hydrostatic Testing on Waterproof Seams
Every batch of heat-sealed TPU wet pockets undergoes hydrostatic head pressure testing (AATCC 127). Clamped samples must withstand a water column pressure exceeding 10,000mm $H_2O$ with zero droplet penetration along welded seam perimeters.
4.4 Antimicrobial Silver-Ion Textile Treatments
To eliminate odor-causing bacteria on a cellular level, Senszx applies silver-ion antimicrobial coatings (such as Sanitized® or SILVADUR™) to interior lining textiles. Verified under AATCC 100 testing, treated fabrics inhibit 99.4% of bacterial colonization over 50 wash cycles.
5. High-Performance Athletic Materials: Oxford, Cordura, Ripstop & Neoprene
Sports duffels are subjected to aggressive abrasion: tossed into metal gym lockers, dragged across athletic turf, and dropped onto wet asphalt. Selecting the appropriate textile weave is vital.
5.1 Comprehensive Material Specification Matrix
Senszx maintains mill-direct supply agreements with certified global textile leaders:
| Material Classification | Polymer Base & Weave Geometry | Weight & Backing Lamination | Martindale Abrasion (Rubs) | Structural Function in Sports Bags |
|---|---|---|---|---|
| 900D High-Tenacity Oxford | 100% High-Tenacity Polyester | 310g/m²; 0.12mm Double PU backing | >18,000 Rubs | The industry workhorse for premium gym duffels: excellent tear strength, smooth print surface. |
| 1200D Heavy Oxford | 100% Polyester Heavy Weave | 380g/m²; Double PU backing + C0 DWR | >24,000 Rubs | Heavy-duty sports team bags, abrasion-resistant side panels, structured end walls. |
| 1680D Ballistic Nylon | High-Tenacity Polyamide, 2x2 Basketweave | 420g/m²; 0.15mm Polyurethane film | >30,000 Rubs | Bottom base boot, locker room scuff panels, heavy cleat compartments. |
| 500D Cordura Nylon 6.6 | Air-Jet Textured Polyamide 6.6 | 240g/m²; C0 DWR + Double PU | >25,000 Rubs | High-end technical tactical gym duffels, CrossFit training packs. |
| 420D Diamond Ripstop Nylon | High-Tenacity Nylon with Ripstop Grid | 180g/m²; Water-repellent PU | >14,000 Rubs | Lightweight active bags, collapsible packing duffels, internal divider walls. |
| 2.5mm Laminated Neoprene | Closed-Cell Chloroprene + Nylon Jersey | 450g/m²; Soft cushioned core | >12,000 Rubs | Boutique yoga duffels, luxury wellness fitness totes, soft-touch lifestyle carriers. |
Review our comprehensive textile guides on 600D vs 900D vs 1680D polyester, what is Cordura fabric, and our complete custom fabric catalog.
5.2 Mechanical & Physical Textile Property Comparison
Below is an exhaustive laboratory comparison of the primary shell textiles used across Senszx custom sports bag programs:
| Mechanical / Physical Property | 900D Oxford Polyester | 1200D Heavy Oxford | 1680D Ballistic Nylon | 500D Cordura Nylon | 420D Diamond Ripstop | 2.5mm Neoprene |
|---|---|---|---|---|---|---|
| Yarn Tenacity (g/denier) | 6.4 g/d | 6.8 g/d | 8.5 g/d | 8.8 g/d | 7.8 g/d | N/A (Foam Core) |
| Tensile Warp Strength (N) | 1,650 N | 2,150 N | 2,850 N | 1,850 N | 1,250 N | 350 N |
| Tensile Weft Strength (N) | 1,350 N | 1,850 N | 2,450 N | 1,650 N | 1,100 N | 320 N |
| Tongue Tear Strength (N) | 180 N | 240 N | 380 N | 280 N | 140 N | 65 N |
| Martindale Abrasion (Rubs) | >18,000 | >24,000 | >30,000 | >25,000 | >14,000 | >12,000 |
| Hydrostatic Water Head (mm) | 1,200 mm | 1,500 mm | 1,500 mm | 1,500 mm | 1,500 mm | Impermeable |
5.3 Eco-Friendly Recycled Synthetics (GRS Certified rPET)
Global athletic apparel brands are prioritizing circular sustainability. Senszx supplies 100% Global Recycled Standard (GRS) certified 600D and 900D rPET polyester textiles manufactured from recycled post-consumer water bottles, complete with full Transaction Certificate (TC) documentation.
5.4 Base Boot Lamination: 1680D Ballistic Nylon vs. TPU Tarpaulin
The bottom base panel of an athletic gym bag rests on damp locker room tiles and wet gym floors:
- 1680D Ballistic Nylon Boot: Laminated with an extra-heavy 0.20mm PU backing, delivering exceptional tear strength and puncture resistance against locker room wire grates.
- Seamless 840D TPU Tarpaulin Base: Creates a completely non-porous rubberized bottom pan that prevents liquid absorption and can be wiped clean with a sanitizing cloth.
5.5 Sustainable Packaging: Recycled LDPE Polybags & Flexo Inks
Senszx enforces eco-conscious packaging standards for international retail delivery:
- 100% GRS Recycled Low-Density Polyethylene (LDPE) Bags: Printed with non-toxic, water-based flexographic inks featuring multilingual legal suffocation warnings.
- FSC-Certified Master Cartons: Constructed from responsibly managed forestry pulp with 100% biodegradable corrugated fluting.
6. Hardware & Zipper Mechanics: #8/#10 Heavy-Duty Zippers & Swivel Snap Hooks
Hardware on sports bags experiences intense rotational shear and lateral tensile forces when the duffel is loaded with 15kg to 25kg of athletic gear.
Critical Sports Bag Hardware & Fastener Matrix
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| MAIN U-SHAPED LID ZIPPER] #10 Heavy-Duty Continuous Nylon Coil with Dual Auto-Lock Sliders | - |
| SHOE COMPARTMENT ZIPPER] #8 Water-Resistant Reverse Coil with Ergonomic Rubber Pullers | - |
| SHOULDER STRAP HOOKS] Die-Cast Zamak 5 Zinc Alloy Swivel Snap Hooks | Tensile >950N |
| SIDE ADJUSTER BUCKLES] Virgin Molded Polyoxymethylene (POM/Acetal) | Tensile >850N |
| LOAD-BEARING WEBBING] 100% High-Tensile Seatbelt Weave Polyester (38mm / 50mm x 1.4mm) | - |
6.1 Hardware Specification Ledger for Athletic Duffels
Below is an engineering specification ledger of critical load-bearing hardware items configured for Senszx sports bag programs:
| Item Code | Hardware Component | Material & Metallurgy | Finish / Coating | Tensile Break Threshold | Function in Bag Architecture |
|---|---|---|---|---|---|
| SPT-HW-01 | Heavy Swivel Snap Hook (38mm) | Die-Cast Zamak 5 Zinc Alloy | Matte Gunmetal PVD Electroplate | >1,150 N (117 kgf) | Detachable shoulder strap anchor. |
| SPT-HW-02 | Welded Heavy Steel D-Ring (38mm) | Solid Carbon Steel Wire (4.5mm) | Matte Black E-Coat | >1,600 N (163 kgf) | Side wall shoulder strap attachment point. |
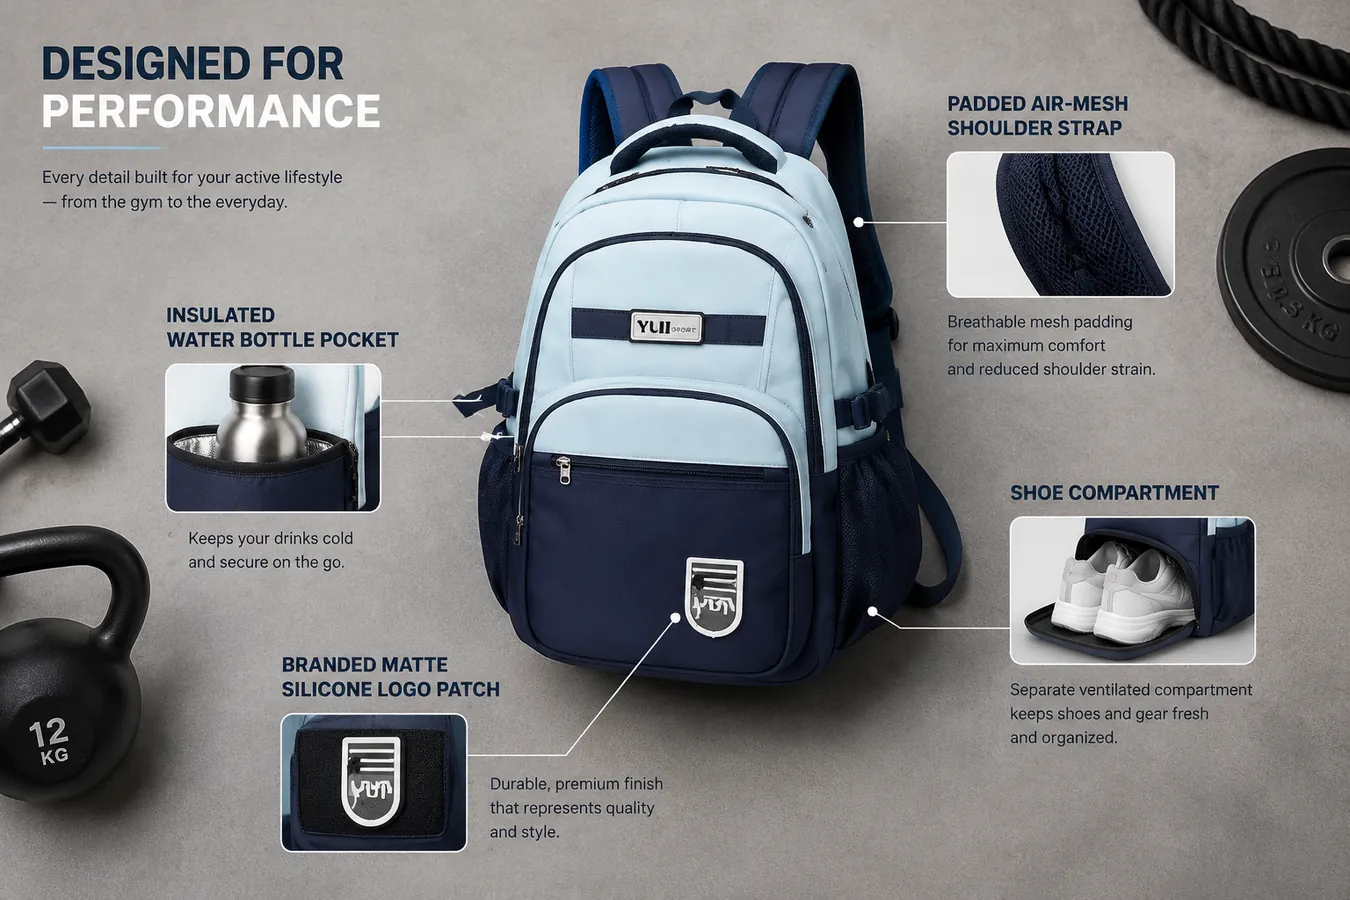
| SPT-HW-03 | Ergonomic Shoulder Strap Pad | 3D Air-Mesh + 8mm High-Density EVA | Breathable Mesh Contact | Impact load >450 N | Cushions heavy shoulder carry payload. |
| SPT-HW-04 | Main U-Lid Opening Zipper | #10 Continuous Nylon Coil + Sliders | Matte Black / Metal Teeth | Cross-tensile >750 N | Wide-mouth main gear compartment opening. |
| SPT-HW-05 | Shoe Compartment Reverse Zip | #8 Reverse Coil with PU Tape | Matte Water-Resistant | Cross-tensile >550 N | Side shoe tunnel opening. |
| SPT-HW-06 | Molded Silicone Brand Patch | 3D Multi-Layer Molded Silicone | Pantone Color Matched | Heat bond >15 N/cm² | Exterior brand logo application. |
| SPT-HW-07 | Insulated Bottle Elastic Mesh | 450g/m² Heavy Polyester Mesh + Cord | Matte Black | Tensile hold >180 N | Exterior water bottle / protein shaker holster. |
Review our complete hardware specifications in our custom zipper pullers and buckles guide.
6.2 Custom Molded Silicone Logos & Reflective Detailing
In performance activewear branding, exterior logo applications must withstand flexing, washing, and friction:
- High-Definition 3D Molded Silicone Badges: Multi-color silicone injection molds applied via high-temperature vulcanized thermal bonding (>180°C), providing vivid, durable relief branding that will not crack or peel.
- Reflective 3M Scotchlite Heat-Transfer Accents: Strategically positioned along shoulder strap webbing and side pocket borders, enhancing pedestrian visibility during pre-dawn or night urban commutes.
6.3 Dynamic Handle Wraparound Reinforcement
Top grab handles on sports duffels must never terminate directly on the upper fabric seam:
- Continuous Base-Wrap Webbing: 38mm seatbelt-grade polyester webbing originates from the top carry handle, extends continuously down both side walls, wraps completely underneath the bottom structural boot, and forms the opposing handle loop.
- Computerized 42-Stitch 'X-Box' Bartacks: Applied at every 100mm interval, ensuring that heavy 25kg athletic payloads are cradled from the base up with zero vertical peel stress on top horizontal seams.
7. Multi-Stage Quality Control, 5,000-Cycle Handle Jerk & Wet-Pocket Leakage Testing
Quality control on sports duffels requires validating mechanical strength and watertight barrier integrity:
Senszx 6-stage Quality Architecture
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| GATE 1 | IQC] Raw Material Testing: 4-Point Fabric Check, Colorfastness, Hardware Pull |
| v | - |
| GATE 2 | PRE-PROD] Pre-Production Sample Sign-Off & Automated CNC Cut Dimensional Check |
| v | - |
| GATE 3 | IPQC] In-Process QC: Stitch Density (7-8 SPI), Seam Binding, Cyclic Bartacks |
| v | - |
| GATE 4 | 100% QC] 100% Semi-Finished Structural Inspection & Cleanliness Audit |
| v | - |
| GATE 5 | FQC] Final Random Inspection (ISO 2859-1 / AQL 2.5 Major, 4.0 Minor, Drop Test) |
| v | - |
| GATE 6 | LOGISTICS] Carton Palletization, Desiccant Check, Barcode & Container Loading Audit |
7.1 Laboratory Testing Standards for Athletic Sports Bags
| Physical Laboratory Test | Testing Equipment & Applied Mechanical Force | Industry Minimum Standard | Senszx Quality Standard (Exceeds Industry) |
|---|---|---|---|
| Dynamic Handle & Strap Jerk | Reciprocating eccentric cam jerk tester; bag loaded with 20.0 kg payload. | 2,500 cycles at 30 jerks/min without anchor tear. | 5,000 Continuous Cycles with zero seam elongation or hardware fatigue. |
| Wet Pocket Hydrostatic Leak Test | Filled with 2.0 liters of water and suspended for 24 hours over dry blotting paper. | Zero moisture bleed through welded TPU seams. | 100% Watertight (Zero Seepage) across all thermal-welded seams. |
| Shoe Tunnel Zipper Fatigue | Lateral cross-tension zipper tester under 140N constant pull-force. | 2,500 open/close cycles without tooth failure. | 5,000 Cycles with smooth action force remaining <3.8N. |
| Fabric Martindale Abrasion | Martindale abrasion tester (ISO 12947-2) under 12 kPa pressure. | 15,000 rubs without yarn breakage. | >25,000 Rubs for 900D/1200D Oxford and 1680D Ballistic nylon. |
| Hardware Salt Spray Corrosion | Heated salt spray chamber (ASTM B117); 5% neutral NaCl fog at 35°C for 48 hours. | No red rust; minor surface tarnishing permitted. | Zero Red Rust, Zero Pitting, Zero Flaking on metal snap hooks and D-rings. |
| Metal Detection Scanning | Dual-aperture 9-point calibrated metal detection conveyor tunnel. | 100% of finished goods inspected. | Zero Tolerance (AQL 0.0) for broken needle fragments or sharp metal debris. |
Review our complete inspection procedures on our dedicated quality control page.
7.2 In-Process Workmanship Defect Prevention Matrix for Sports Duffels
Below is a shop-floor defect prevention matrix utilized by Senszx IPQC auditors during sports bag production:
| Potential Workmanship Defect | Root Industrial Cause | Senszx Shop-Floor Preventive Measure |
|---|---|---|
| Shoe Tunnel Seam Tearing | Heavy shoes pulling on single-stitched tunnel join. | Double-stitching tunnel join with bonded nylon #69 thread and 22mm binding. |
| TPU Wet Pocket Leaking | Inadequate welding temperature or ultrasonic dwell time. | Calibrating automated pneumatic RF welders with computerized temperature sensors. |
| Handle Webbing Pull-Out | Webbing stitched into top panel seam without under-wrap. | Mandating continuous seatbelt webbing running under base with 42-stitch bartacks. |
| Ventilation Eyelet Looseness | Hole punched too large in fabric panel before crimp. | Automated precision die-punching matching exact 12mm eyelet flange dimensions. |
| Main U-Lid Zipper Puckering | Manual feed rate variation around U-curve corner. | Utilizing specialized cylinder-bed walking-foot machines with curved guide attachments. |
7.3 Handle Jerk Testing & Dynamic Load Path Validation
When an athlete hoists a 20kg loaded gym duffel abruptly into a vehicle trunk, the instantaneous dynamic shock force exceeds 650N. Senszx validates all carry handles on automated eccentric cam jerk testers for 5,000 continuous cycles at 30 jerks/min, verifying zero thread breakage and zero rivet looseness.
8. Standard Allowed Minutes (SAM), Line Balancing & Industrial Engineering
Producing high-performance sports duffels with shoe tunnels and wet/dry pockets requires balanced Standard Allowed Minutes (SAM) across specialized workstations:
Senszx Industrial Manufacturing Capacity Profile
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| Synchronized Active Sewing Lines | 100 Dedicated Industrial Production Lines |
| Specialized Heavy-Duty Machine Fleet | 350+ Specialized Machines (Walking-Foot/CNC/Post-Bed) |
| Master Sports Bag Crafting Workforce | 260+ Full-Time Industrial Seamstresses & Technicians |
| Monthly Mass Production Capacity | 120,000 to 180,000 Athletic Duffels & Backpacks |
| Standard Mass Production Turnaround | 20 Calendar Days (500 to 5,000 pcs) |
| Parallel Active Project Capacity | 30 to 45 Multi-SKU Production Programs in Parallel |
8.1 Detailed SAM Breakdown for a 45L Technical Sports Duffel
| Station # | Assembly Operation Description | Machine Type Assigned | SAM (Minutes) | Critical Quality Checkpoint |
|---|---|---|---|---|
| ST-01 | Sub-assembly: Inverted shoe tunnel 210D lining & laser eyelet install | Eyelet Press & Lockstitch | 3.2 min | Eyelet crimp tightness, smooth lining seam |
| ST-02 | Sub-assembly: Ultrasonic thermal welding of TPU wet/dry pocket | High-Frequency TPU Welder | 2.5 min | 100% hermetic weld, zero pinholes |
| ST-03 | Sub-assembly: Front organizer panel with shaker bottle elastic mesh | Single-Needle with Binding Guide | 2.8 min | Mesh tension uniformity, zipper glide |
| ST-04 | Sub-assembly: Padded air-mesh shoulder strap EVA lamination & webbing | Walking-Foot with Edge Guide | 3.5 min | Centered 38mm seatbelt webbing, air-mesh |
| ST-05 | Sub-assembly: Computerized 42-stitch cyclic bartacks on handle anchors | CNC Pattern Bartacker | 1.8 min | X-box coordinate alignment, thread lock |
| ST-06 | Main assembly: U-shaped top lid #10 zipper installation & piping | Walking-Foot Compound Feed | 4.5 min | Symmetrical U-curve, smooth double slider |
| ST-07 | Main assembly: Side shoe compartment gusset joining & zipper stitch | Cylinder-Bed Synchronized Feed | 4.2 min | Smooth corner radius curves, zero puckering |
| ST-08 | Main assembly: 3D joining of cylinder end caps to main body | Post-Bed Double-Needle | 5.8 min | Parallel top-stitching, symmetry tolerance <2mm |
| ST-09 | Final assembly: Internal heavy herringbone seam edge binding | Cylinder-Bed Binding Machine | 4.8 min | 100% raw edge encapsulation, zero fraying |
| ST-10 | Finishing: 100% thread trimming & structural cosmetic inspection | Dedicated Inspection Table | 2.5 min | Cleanliness, zipper pull check, shape memory |
| ST-11 | Packaging: Metal detection tunnel & 5-ply Kraft master cartoning | Calibrated Metal Tunnel | 1.2 min | Zero metal fragments, barcode label verify |
| TOTAL | Complete Manufacturing Cycle Per Sports Duffel | 11 Integrated Stations | 36.8 min | Daily Output per 20-Person Line: ~290 units |
8.2 Ergonomic Padded Shoulder Strap Assembly & Air-Mesh Ventilation
Sports duffels carried over one shoulder with a 20kg payload require advanced ergonomic padding:
- Multi-Density Strap Core: 8mm closed-cell EVA foam core laminated to 5mm perforated open-cell foam distributes point pressure across the shoulder cap.
- Breathable 3D Spacer Mesh: Woven from moisture-wicking polyester filaments that allow air to circulate beneath the strap pad, preventing sweat saturation.
- Dual Articulating Swivel Hooks: Zamak zinc alloy snap hooks with 360-degree swivel bearings prevent webbing twist during fast walking or airport transit.
9. Single-Track 500 MOQ Economics & 100% Credited Prototyping Program
For fitness lifestyle startups, gym apparel brands, and collegiate athletic merchandise programs, managing inventory risk is critical. Traditional factories demand 2,000 to 3,000-unit minimums that tie up working capital.
Senszx eliminates this barrier through our Single-Track OEM/ODM MOQ Structure:
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| Senszx Sourcing Economics & Flexibility | - |
| Single-Track OEM/ODM MOQ | 500 Pieces Per Style / Colorway |
| Prototyping Turnaround | 3 to 5 Business Days |
| Mass Manufacturing Lead Time | 20 Calendar Days (500 to 5,000 units) |
| Development Fee Program | 100% Prototyping Fee Credited Back on Bulk Order |
9.1 The Structured Development Fee Credit-Back Program
For visionary brands launching innovative new athletic bag silhouettes:
- Upfront Prototyping Investment: A structured engineering fee covering complete CAD pattern drafting, specialized material sourcing, acrylic cutting templates, and up to 3 iterative rounds of physical prototyping.
- 100% Invoice Credit-Back: When the client approves the golden prototype and places their commercial mass production order of 500+ units, 100% of the initial development fee is credited directly back against the mass production invoice.
- Zero-Risk Commercial Scaling: This framework gives expanding brands direct access to Tier-1 industrial engineering, certified materials, and master sample technicians without requiring upfront multi-thousand-unit inventory exposure.
To explore stock options, browse our wholesale backpacks in stock section or review our custom bag product catalog.
9.2 Direct Unit Cost Breakdown for a 45L Technical Sports Duffel
Understanding direct manufacturing cost drivers in sports bag production:
- Outer Shell & Base Textiles (900D Oxford / 1680D Ballistic): Accounts for approximately 35% to 40% of FOB cost.
- Shoe Tunnel, Linings & TPU Wet Pocket Membrane: Accounts for 16% to 20% of cost.
- Hardware, Zippers & Ventilation Eyelets (Zamak Hooks, #10 Coil): Accounts for 18% to 22% of cost.
- Direct Sewing Labor (36.8 Standard Allowed Minutes): Accounts for 20% to 24% of cost.
- Packaging, Quality Inspection & Port Drayage: Accounts for 6% to 8% of cost.
9.3 Total Cost of Ownership (TCO) vs Lowest Quoted Unit Price
Procurement teams evaluating sports bag manufacturers must look past initial low-bid FOB quotations. Sourcing through unverified middlemen often results in unapproved textile downgrades (substituting 900D Oxford with low-tenacity 600D fabric), leaky stitched wet pockets that ruin consumer electronics, broken zipper sliders on shoe compartments, and high warranty return rates (>4.2%). Partnering directly with Senszx delivers predictable 20-day production schedules, certified BSCI working conditions, zero material substitutions, sub-0.25% warranty return rates, and a 22% to 28% net financial advantage in Total Cost of Ownership (TCO). Review our comprehensive custom backpack cost breakdown for detailed pricing models.
9.4 Capsule Colorway Dropping for Activewear & Gym Brands
Fitness lifestyle brands rely on seasonal color drops (e.g., Triple Black, Sage Green, Dusty Rose, Cobalt Blue):
- Core Substrate Standardization: Senszx standardizes all interior shoe tunnels, wet pockets, zippers, and binding tapes across all SKUs, allowing brands to split a 500-unit order across multiple shell colorways with zero small-batch surcharge penalties.
10. Sourcing Playbook, RFQ Formulation & Factory Audit Scorecard
Global sportswear brands execute custom athletic duffel programs with Senszx through our disciplined 6-phase procurement workflow:
The 6-phase Factory-direct Sourcing Playbook
| Parameter / Specification Stage | Factory Engineering Protocol & Technical Details |
|---|---|
| PHASE 1 | TECHNICAL RFQ & FEASIBILITY REVIEW] Timeline: Days 1-2 |
| Brand submits 2D CAD tech pack, target dimensions, material specs, target FOB price. | - |
| Factory engineering team performs DFM stress-point analysis and provides detailed BOM quotation. | - |
| PHASE 2 | CAD PATTERN DRAFTING & MATERIAL SOURCING] Timeline: Days 3-4 |
| Digitizing 2D pattern geometry in Optitex CAD software; preparing acrylic cutting templates. | - |
| Procuring master textile swatches, zipper chains, custom hardware samples, and foam cores. | - |
| PHASE 3 | PHYSICAL PROTOTYPE SAMPLING & ITERATION] Timeline: Days 5-8 |
| Master sample technicians hand-craft 1st physical prototype in dedicated sample room. | - |
| High-res photo/video review with brand; dispatching sample via express courier (DHL/FedEx). | - |
| Client testing and review; executing up to 2 refined iteration rounds if required. | - |
| PHASE 4 | GOLDEN SAMPLE APPROVAL & CONTRACT SIGN-OFF] Timeline: Days 9-10 |
| Client signs off on Golden Master Sample and formal Master Production Specification Sheet. | - |
| Finalizing 500+ unit purchase order; deposit confirmation; locking mass production schedule. | - |
| PHASE 5 | AUTOMATED CUTTING & MASS SEWING PRODUCTION] Timeline: Days 11-28 |
| Gate 1 IQC textile inspection and automated multi-ply CNC knife cutting. | - |
| 100 synchronized sewing lines execute assembly under continuous roving IPQC inspection. | - |
| 100% semi-finished trimming, structural integrity checks, and clean-line finishing. | - |
| PHASE 6 | FINAL FQC AUDIT, PACKAGING & CONTAINER LOADING] Timeline: Days 29-30 |
| Chief Quality Auditor executes ISO 2859-1 (AQL 2.5/4.0) random sampling inspection. | - |
| Metal detection tunnel scanning; virgin LDPE polybag packaging; 5-ply Kraft master cartoning. | - |
| Direct ocean container drayage loading at factory docks; issuing full Bill of Lading (B/L). | - |
10.1 Diagnostic Questions for Sports Bag Sourcing Audits
When evaluating prospective sports duffel manufacturers, procurement directors should ask these targeted technical questions:
- "How do you seal the seams of your internal wet/dry pockets, and do you perform 100% hydrostatic water pressure testing?"
- "What specific webbing wraparound construction do you utilize on the main carry handles to prevent handle tear-out under a 20kg payload?"
- "What is your documented in-line inspection protocol for verifying metal ventilation grommet crimp tightness and eyelet smoothness?"
- "Can you conduct an unannounced live video walkthrough of your CNC cutting room, sewing lines, and in-house testing lab within the next 30 minutes?"
- "How do you test anti-microbial silver-ion treated lining fabrics for wash durability (AATCC 100) and odor suppression?"
- "What is your Standard Allowed Minutes (SAM) calculation for joining 3D cylindrical end caps on post-bed machines?"
- "What class of air-filtration and static elimination do you maintain during final packing to prevent particulate contamination?"
- "How do you grade the keystone taper on your internal shoe tunnels to accommodate US Men's size 14 athletic footwear without binding?"
10.2 CAD Master Pattern Nesting & Multi-Ply Cutting Protocols
In high-volume sports duffel manufacturing, pattern accuracy directly controls production efficiency:
- Digitized Cylindrical End-Cap Grading: Symmetrical 360-degree round end-caps require precise perimeter matching ($P = 2\pi r$) within $\pm 0.5\text{mm}$ to prevent twisting or puckering during post-bed double-needle sewing.
- Automated CNC Reciprocating Knife Cutting: 50 layers of heavy 900D/1200D Oxford are cut simultaneously with automated vacuum hold-down tables, achieving over 95.4% material utilization and reducing scrap waste.
- Laser-Cut Acrylic Sewing Jigs: Clear acrylic positioning templates with engraved reference notches guide sewing line operators during high-speed assembly.
10.3 Global Supply Chain Traceability & Environmental Compliance
Modern sportswear brands require complete chemical and environmental transparency across their supply chains:
- GRS Transaction Certificates (TC): Sourcing recycled polyester with certified lot traceability from post-consumer PET flake suppliers, guaranteeing full chain-of-custody documentation.
- OEKO-TEX Standard 100 & Zero Hazardous Discharge: Verifying zero toxic heavy metals, zero alkylphenol ethoxylates (APEOs), zero formaldehyde, and zero banned azo colorants in textile dyeing processes across all certified fabric mills.
10.4 Production Milestone Schedule: From CAD Release to Port Drayage
To maintain strict 20-day mass production timelines, Senszx tracks production milestones across digitized Gantt scheduling systems:
- Days 1-2: Finalizing CAD pattern cut files, creating laser-cut acrylic templates, and releasing purchase orders to certified raw material mills.
- Days 3-5: Gate 1 IQC inspection of incoming 900D/1200D fabric bolts (4-point inspection system), hydrostatic water column testing, and 24-hour tension-free fabric relaxation.
- Days 6-8: Automated multi-ply CNC knife cutting and sub-assembly kitting (bundling cut panels with matched thread and hardware).
- Days 9-17: Synchronized sewing line assembly across 100 dedicated lines under continuous roving IPQC inspection.
- Days 18-19: 100% semi-finished trimming, structural cleanliness audit, and metal detection tunnel scanning.
- Day 20: Chief Quality Auditor executes ISO 2859-1 (AQL 2.5/4.0) final inspection, carton palletization, and ocean container drayage dispatch.
10.5 Global Maritime Transit Gateways & Port Logistics
Senszx coordinates direct container loading from our factory loading bays to North China’s primary international seaport (Tianjin Port, Xingang) and Southern export hubs (Shenzhen and Guangzhou Ports), connecting directly to global logistics corridors with full automated AMS and ISF customs documentation, comprehensive Bill of Lading (B/L) issuance, and seamless inland drayage:
| Global Destination Gateway | Average Ocean Transit Time | Customs Clearance & Inland Drayage | Total Factory-to-Warehouse Window |
|---|---|---|---|
| US West Coast (Long Beach / Los Angeles / Tacoma) | 14 to 18 Days | 3 to 5 Days (Automated ISF/AMS filing) | 18 to 23 Calendar Days |
| US East Coast (New York / Savannah / Charleston) | 28 to 34 Days (via Panama Canal) | 3 to 5 Days | 32 to 39 Calendar Days |
| Northern Europe (Rotterdam / Hamburg / Antwerp) | 26 to 32 Days | 3 to 4 Days (EU Import VAT & EORI) | 30 to 36 Calendar Days |
| United Kingdom (Southampton / Felixstowe / London) | 28 to 34 Days | 3 to 4 Days | 32 to 38 Calendar Days |
| Middle East / GCC (Jebel Ali, Dubai / Dammam) | 16 to 22 Days | 2 to 4 Days (SABER / SASO clearance) | 19 to 26 Calendar Days |
| Australia (Sydney / Melbourne / Fremantle) | 14 to 18 Days | 2 to 3 Days | 17 to 22 Calendar Days |
10.6 Automated Customs Filing & Tariffs Optimization
Our international logistics department provides comprehensive export documentation for US and European customs compliance:
- Harmonized Tariff Schedule (HTS) Classification: Providing precise HTS code mapping (e.g., HTS 4202.92 for textile travel and sports bags) to ensure accurate duty calculations.
- Automated ISF (10+2) & AMS Filing: Ensuring timely electronic filing prior to vessel departure to eliminate costly US Customs entry holds or inspection demurrage fees.
- DDP (Delivered Duty Paid) Direct-to-3PL Service: Managing the entire freight chain, customs brokerage, import duties, and final inland lift-gate delivery directly to your domestic 3PL warehouse or Amazon FBA fulfillment center.
- Anti-Crush Master Carton Stacking: 5-ply double-wall Kraft master cartons are engineered with an Edge Crush Test rating of ECT 44 and Mullen burst strength of 275 lbs/in², supporting up to 8-high vertical pallet stacking inside 40ft High Cube containers without side-wall buckling. Every carton is sealed with heavy fiberglass-reinforced water-activated Kraft tape to prevent pilferage and moisture ingress during intermodal rail and ocean transit.
Direct Sourcing Comparison Matrix: How Suppliers Stack Up
| Sourcing Dimension | Tier-1 Factory-Direct (Senszx) | Small Cottage Workshop | Sourcing Trading Company | Virtual Sourcing Broker |
|---|---|---|---|---|
| Machinery Infrastructure | 100 Synchronized Lines, heavy walking-foot, CNC knife cutters, testing lab. | 5-10 generic flatbed sewing machines; manual hand cutting. | Office showroom only; zero manufacturing machinery. | Home office / laptop; zero assets. |
| Prototyping Turnaround | 3 to 5 business days with in-house CAD master pattern makers. | 15 to 25 days; relies on manual paper patterns. | 20 to 30 days; must relay to external workshops. | 25 to 35+ days; multi-tiered handoffs. |
| Mass Production Lead Time | 20 calendar days (500 to 5,000 units). | 45 to 60+ days; severe labor bottlenecks. | 35 to 50 days; vulnerable to factory rescheduling. | Unpredictable; frequent shipping delays. |
| In-Line Quality Control | 6-Gate System (IQC, IPQC, 100% semi-finished, FQC / AQL 2.5). | Casual visual check by sewing operators. | Pre-shipment inspection (PSI) only at 100% completion. | Relies entirely on unverified supplier claims. |
| Lab Stress Testing | In-house physical lab (5,000-cycle handle jerk, drop tower, salt spray). | Zero physical testing equipment. | None; charges extra for external lab reports. | None. |
| Compliance Certifications | BSCI, ISO 9001/14001/45001, CPSIA, REACH, Prop 65. | None; uncertified working conditions. | Holds trading certificates; underlying factories unverified. | None. |
| Cost Structure & Transparency | Direct cost-plus BOM pricing; zero middleman markups. | Low initial quote; hidden material downgrades. | 15% to 35% hidden trading margin markup. | 10% to 20% commission layered over marked-up cost. |
| MOQ Flexibility | 500 pcs/style (100% Development Fee credit-back). | 100-300 pcs, but lacks quality control. | 1,000 to 3,000 pcs minimum. | 2,000+ pcs minimum. |
Summary & Next Steps: Partner Directly with Senszx
In the competitive global marketplace of athletic bags, gym duffels, and fitness accessories, your sports bag is the physical representation of your brand's commitment to athletic performance, hygiene, and durability. By partnering directly with Senszx, you eliminate intermediary markups, protect design intellectual property, ensure pristine sample-to-bulk fidelity, and secure a resilient, scalable 100-line manufacturing infrastructure engineered for athletic excellence.
Initiate Your Custom Sports Bag Development Today
Contact our senior engineering team to review your technical drawings, optimize your Bill of Materials, receive a direct factory quotation, and dispatch your rapid 3-5 day prototype sample:
- Email Direct: [email protected]
- WhatsApp / Direct Line: +86 17331531825
- Request a Prototype: Get a Free Sample
- Submit Technical RFQ: Contact Our Engineering Team
- Explore Factory Background: Read Our Factory Story
- Review Quality Procedures: Quality Control Floor
- Inspect Cutting Facilities: Fabric Cutting Workshop
- Review Certifications: BSCI & ISO Standards
- Check Logistics & Terms: Payment & Shipping Information
- Browse Product Range: Custom Bag Product Catalog
- Custom Backpack Manufacturing: Custom Backpacks Factory
- Custom Travel Bags: Custom Travel Bags Factory
- Custom Gym Bags: Custom Gym Bags Factory
- Custom Tactical Bags: Custom Tactical Bags Factory
- Custom Tote Bags: Custom Tote Bags Factory
Hi, I'm Senszx Bag Manufacturer, Hope You Like This Blog Post.
With more than 20 years of experience in OEM/ODM/Custom luggage and bag, I'd love to share with you the valuable knowledge related to luggage and bag products from a top-tier Chinese supplier's perspective.
Senszx Factory
Est. 2006 · Baigou, China
Related articles
How to Choose the Right Materials for Travel Bags: The Complete Manufacturer Guide
A comprehensive B2B engineering guide to selecting travel bag materials: comparing polyester, nylon, Oxford, canvas, TPU coatings, hardware, and structural interlinings across durability, GSM, abrasion, and manufacturing cost.
Bulk Backpacks: The Complete Wholesale Buying Guide for 2027
How brands, distributors, schools and charities buy backpacks in bulk: sourcing paths, styles, fabrics, customization, unit price drivers, MOQ, lead times, QC and shipping.
Wholesale Toiletry Bags: The Complete Sourcing Guide for 2027
How travel brands, grooming labels, retailers and distributors source toiletry bags in bulk: styles, materials, customization, MOQ, pricing, QC and shipping.
Get a Custom Bag Quote from Our China Factory
Our sales team is online around the clock and usually replies within the hour.
Email
[email protected]Factory
Qinzheng Road No.89, New Industry Zone, Baigou Town
Baoding City, Hebei Province 074004, China